6 Silicone Tracker Cover Design Details That Affect Fit, Retention, and Moldability
- Share
- publisher
- FromRubber
- Issue Time
- Oct 19,2026
Summary
Six design details decide whether a silicone tracker cover fits, holds and can be moulded consistently. The article connects each detail to a behaviour and to a validation method, and shows where the details interact.
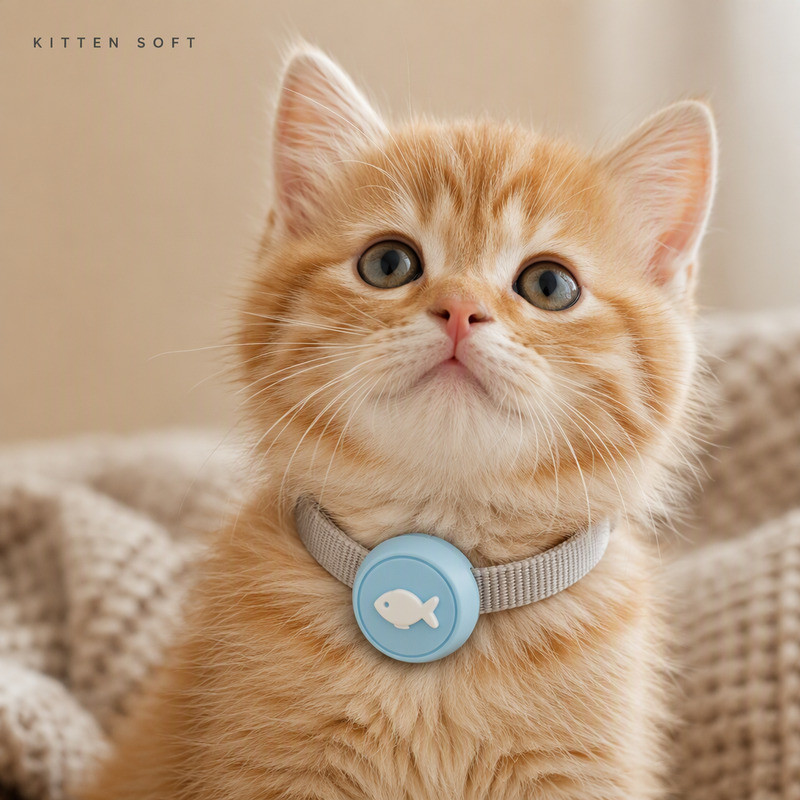
Small silicone tracker covers fail in ways that look disproportionate to the change that caused them. A 0.4 mm difference at a corner radius turns a firm fit into a rattle. A lip that is 0.2 mm shorter than drawn releases under a dog’s shake. None of these are material failures, and none of them show up in a rendering.
Six details decide most of the behavior. They are not independent, which is the part that catches teams out: adjusting one to fix a symptom usually moves two others.
Why small parts amplify small errors
In a large molded part, a fraction of a millimeter is absorbed by the surrounding geometry. In a cover the size of a coin, it is a meaningful percentage of the wall, the lip and the cavity. The same shrinkage that is invisible on a 200 mm panel can move a 32 mm cavity enough to change insertion force.
The second amplifier is that the part is elastic. A rigid cover transmits load; a silicone cover stores it. Every dimensional mismatch becomes a local strain, and local strain is what tears rims and relaxes lips. That is why the review has to look at the six details together rather than as a checklist of independent features.
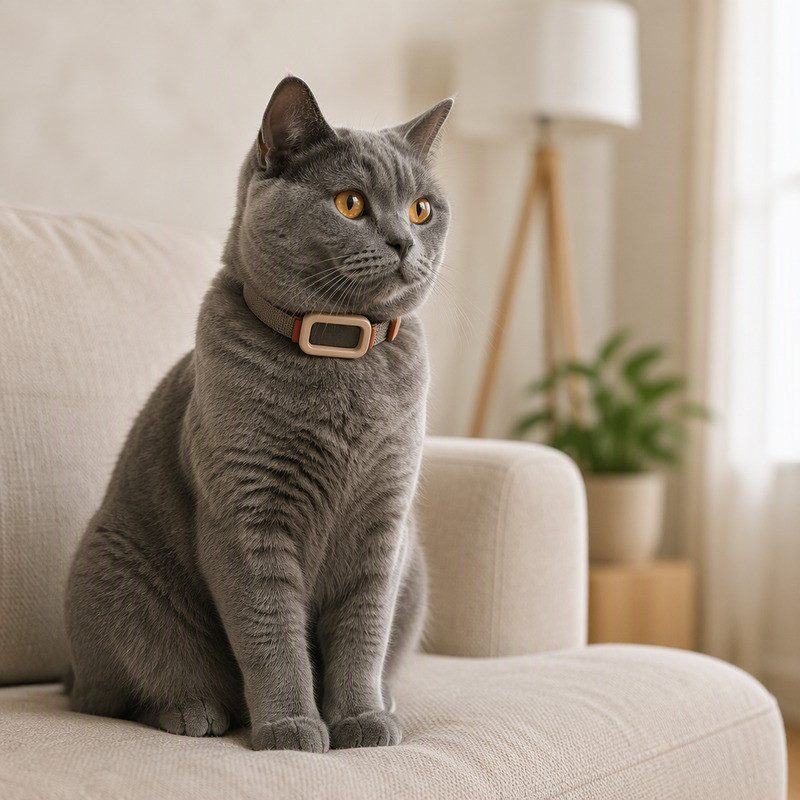
Scale is easier to see on the animal than on the bench. The cover below is small relative to the cat, and the collar is narrow, so the whole assembly is dominated by edge contact rather than by surface area. On a larger dog with a wide collar, the same design has more contact length and behaves differently — not because the silicone changed, but because the ratio of channel length to clearance changed.
Keep that ratio in mind through the six details. It explains why a design that is stable on one collar becomes marginal on another without any change to the part.
Detail one: cavity dimensions and corner radii
The cavity is usually dimensioned from a device drawing, and the drawing usually gives length, width and thickness. Three numbers describe a box. A tracker is not a box: it has rounded corners, a curved back, and often a raised lens or button that sits proud of the nominal face.
Corner radii are where the fit is decided. If the cavity radius is larger than the device radius, the device is held on four flat walls and rocks between them. If it is smaller, the device contacts the cavity at four points and the walls between those points stay unstressed, which looks like a good fit until the device shifts and loads one corner. Either mismatch produces movement that is easy to blame on the material.
| Dimensional problem | What the user notices | What is actually happening |
|---|---|---|
| Cavity 0.3–0.5 mm oversized | Slight rattle, device sits off-center | Device migrates until a corner loads the lip |
| Cavity undersized at corners | Hard to insert, cover bulges | Local overstretch; strain concentrates at the rim root |
| Cavity floor flat, device back domed | Device rocks when pressed | Point contact at the center; lip takes the load |
| Cavity depth short | Device sits proud, lip barely engages | Retention depends on friction alone |
| Port opening misaligned | Cable does not seat, plug scratches housing | Cavity position drifted in the tool |
Detail two: retaining lips, hooks and undercuts
A retaining lip works by overlapping the device face. The overlap is the engagement depth, and the amount the lip must deflect to pass the device is the interference. Retention comes from engagement; removal effort comes from interference and from how the lip is shaped on the way out.
When a lip is too shallow, the cover relies on sidewall friction, and friction falls as the cavity wears and as the silicone takes a set. When a lip is too deep, the removal force rises faster than the retention benefit, because the lip has to be peeled rather than deflected. The useful design move is asymmetric geometry: a generous ramp on the entry side, a squarer face on the retaining side, and a root radius that distributes strain instead of concentrating it at a sharp internal corner.
Hooks and undercuts do the same job more aggressively and cost more in tooling. Any undercut has to be released, either by stretching the part or by a tooling feature. Stretching at ejection loads the lip when the part is still warm and weakest. A sliding core avoids that and adds a parting line, which may land on a visible face.
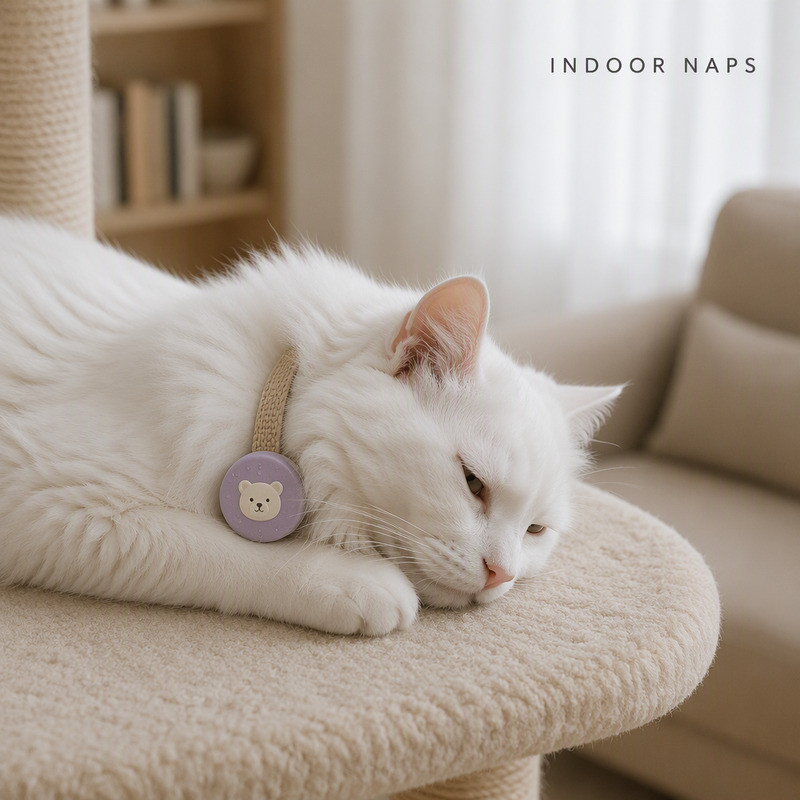
This is why a cover can pass a hand-fit check and fail in a home. A bench test applies one load, briefly, in one direction. A cat lying against a cushion applies a small sideways load for hours, which is exactly the condition that walks a device out of a shallow cavity.
If the retention feature is only engaged by a millimeter, slow loads will find the gap. The lip does not need to be taller; it needs to be engaged at the point where the load acts.
Detail three: collar channel width and contact area
The collar interface has its own dimensions and its own failure mode. A channel that is too wide lets the holder rotate; a channel that is too tight makes installation difficult and compresses the webbing, which then relaxes.
Contact length matters more than contact area on a narrow collar. A short channel on a narrow strap has very little lever arm to resist rotation, so the edge fit has to be close. On a wide collar the same channel length is more stable, but a long channel resists the collar’s curve and lifts at the ends when the collar bends around a neck.
Check for interference with the things that are not the strap: stitching, bound edges, padding and hardware. A holder that fits the webbing perfectly can still be unusable because it cannot pass a stitch line or sit flat against a padded section.
Detail four: wall thickness and local flexibility
Wall thickness is the most adjustable variable in the design and the one most often set by eye. It controls three things at once: how much the cavity can expand during insertion, how much force the rim needs to deflect, and how the part behaves after molding.
Thick sections cool and shrink differently from thin ones. A part with a 4 mm body and a 0.8 mm lip will have a molded geometry that differs from the drawing in both places, and the difference is not uniform. That is the origin of many “the sample fits but the production part does not” reports: the prototype may have been cut from a tool that was adjusted by hand, while production runs the tool as designed.
There is no universal wall thickness to recommend here. What can be said is that the wall should be chosen with the removal frequency and the rim geometry, not in isolation. A cover that is opened daily can use a thinner wall and a longer ramp. A cover installed for a season can use a thicker wall and a shorter ramp, because it only has to survive a few cycles.
Detail five: hardness, recovery and shrinkage
Hardness is quoted because it is easy to measure, and it is a poor predictor on its own. The reasoning is set out in more detail in this note on how rubber hardness affects protection, and it applies unchanged to a cover. Two compounds at the same durometer can differ in tensile strength, elongation at break and compression set, and those differences decide whether a lip returns to its molded shape after being stretched [2][3][4].
Recovery is the one to watch in this product. A compound with slow recovery leaves the cavity slightly larger after each removal, so retention decays in a way that is invisible on the first sample. Compression set describes a related behavior under sustained load: a cover that is squeezed against a collar for weeks may not return fully, and the channel that was snug becomes loose.
Shrinkage then adds a manufacturing dimension. Silicone shrinks by an amount that depends on compound, cure and section, and molded rubber dimensions are therefore specified in tolerance classes rather than exact values [1]. If the critical fit dimensions are not identified and toleranced, shrinkage becomes a surprise rather than a variable.
Detail six: draft, parting lines and demolding
Draft is not decoration. Every vertical wall that has to release needs enough angle to break contact without dragging, and the walls inside a cavity are the hardest to draft because the space is small. A cavity wall with insufficient draft scuffs on ejection and leaves a surface that looks acceptable and grips the device unevenly.
Parting-line placement is a compromise between appearance and function. A line across the outer face may be unacceptable for a branded product; moving it to the edge can put flash on the surface that seats against the device. Flash of 0.1 mm on a cavity floor is enough to stop a device seating, and the symptom — a cover that will not close — looks like a cavity depth problem rather than a molding defect.
Demolding direction deserves a decision early because it fixes the position of every other feature. If the part must release in one direction, any undercut becomes a tooling feature. If it can release in two, the tool gets more complex and the cost moves.
How the six details interact
The matrix below is the useful part of the review. Read across a row to see what a change to one detail does to the others; read down a column to see which details control a given behavior.
| Detail | Tracker fit | Retention | Removal | Moldability | Main validation |
|---|---|---|---|---|---|
| Cavity and corner radii | Direct | Indirect | Indirect | Low impact | Gap measurement at corners |
| Retaining lip and undercut | Indirect | Direct | Direct | High impact | Section cut and cycle test |
| Collar channel and contact | None | Direct | Direct | Medium impact | Sliding and rotation trial on real collars |
| Wall thickness | Direct | Direct | Direct | High impact | Insertion force and recovery check |
| Hardness and recovery | Indirect | Direct | Direct | Medium impact | Compression set and repeat fit |
| Draft and parting line | Indirect | Indirect | Indirect | Direct | Visual and dimensional inspection |
Two patterns are worth noticing. First, almost everything affects removal, which is why removal complaints are so hard to diagnose and so easy to misattribute to hardness. Second, moldability is affected most by the features that also control retention — the lip, the wall and the undercut. That is the real tension in the design, and it is why a design-for-manufacturing review belongs before the CAD is frozen rather than after the first sample.
A review sequence that catches the interactions
- Confirm reference dimensions from a device sample and a real collar, not from listings.
- Mark the critical fit and retention features on the drawing, and give each one a tolerance.
- Review wall sections and demolding direction together, since one constrains the other.
- Choose the compound for recovery and elongation, then confirm hardness.
- Agree inspection points and the method for each, including which features get a section cut.
- Approve the CAD and the prototype validation plan in the same review, so the sample is tested against a stated criterion.
On the first molded samples, test the things that a drawing cannot show: insertion and removal on the actual device, collar installation past the hardware, lateral movement and rotation under a slow sideways load, repeated cycles, visible flash on seating surfaces, and dimensional inspection of the six features above. Then inspect for permanent deformation at the rim root and the cavity corners.
None of this replaces durability testing. It answers a narrower question — does the geometry behave as intended — and it answers it before the tool is adjusted for the wrong reason.
Questions from design reviews
Which dimension matters most?
The cavity corner radius, because it decides where the device contacts the cover and therefore how load is distributed. It is also the dimension most often approximated from a drawing.
Do retaining lips always need undercuts?
No. A lip can retain by overlap alone if the entry side is ramped and the material can deflect. Undercuts increase engagement and tooling complexity together; they are a choice, not a requirement.
Can a harder compound fix a loose fit?
Sometimes, and it changes insertion force and tear risk at the same time. If the looseness comes from an oversized cavity or a short lip, hardness is treating the symptom.
Why do molded parts differ from CAD?
Shrinkage, draft, section-dependent cooling and tool wear all move dimensions. Parts are not wrong because they differ; they are wrong when the difference is outside an agreed tolerance on a feature that matters.
Can moldability be assessed before tooling?
Yes, and it is the cheapest time to do it. Wall transitions, undercuts, draft and parting-line placement can all be reviewed on the CAD, with the caveat that some risks only appear on a molded part.
Functional geometry first, appearance second
Six details, one system. The cavity decides where the device sits, the lip decides whether it stays, the channel decides whether the holder stays, the wall decides how both behave, the compound decides how long that lasts, and the tool decides whether any of it can be made consistently.
Silicone is not a universal fix. It will not compensate for a collar outside the design range, and it does not turn a tracker into a waterproof device.
FromRubber, the export brand of Dongguan Bohao Electronic Technology Co., Ltd., molds custom silicone covers and holders for pet product brands in Dongguan, Guangdong, and reviews these details on the drawing before cutting a tool. If you have a device sample and a collar range, send them with your target use to nani@fromrubber.com or karl@fromrubber.com; WeChat and WhatsApp: +86 186 7621 0913. Related notes on molding practice are collected under silicone product technology, with end-use examples under silicone product applications.
Sources
- ISO 3302-1:2014 — Rubber: Tolerances for products, Part 1: Dimensional tolerances, ISO.
- ASTM D2240-15(2021) — Standard Test Method for Rubber Property: Durometer Hardness, ASTM International.
- ASTM D395-18(2025) — Standard Test Methods for Rubber Property: Compression Set, ASTM International.
- ISO 37:2024 — Rubber, vulcanized or thermoplastic: Determination of tensile stress-strain properties, ISO.