Case Study: Designing a Weatherproof ABS Housing for Outdoor Sensor & Camera
- Share
- publisher
- Suey
- Issue Time
- Nov 14,2025
Summary
This case study follows a weatherproof ABS housing for an outdoor sensor and camera from failure list to IP67 validation. It covers the sealing stack, the UV-stabilised grade, the moulding changes that cut cost by 20 percent, and the test sequence that supported a ten-year outdoor claim.

Case study
The brief was a housing that survives ten years outdoors from -30 °C to +60 °C and holds IP67, at a cost the product could carry. The answer was not a more expensive plastic: it was a sealing stack that fails in a defined order, a UV-stabilised ABS grade, and a moulding revision that removed two operations. The project closed at IP67 with a 20 percent lower unit cost.
- Water enters at cable glands and lid joints, not through the wall: the sealing stack, not the resin, decides IP67.
- UV-stabilised ABS plus a matte texture keeps appearance acceptable without a painting step.
- Cost came out of the process — gate position, wall sections and a moulded gasket groove — not out of the material.
The failure list that defined the weatherproof ABS housing
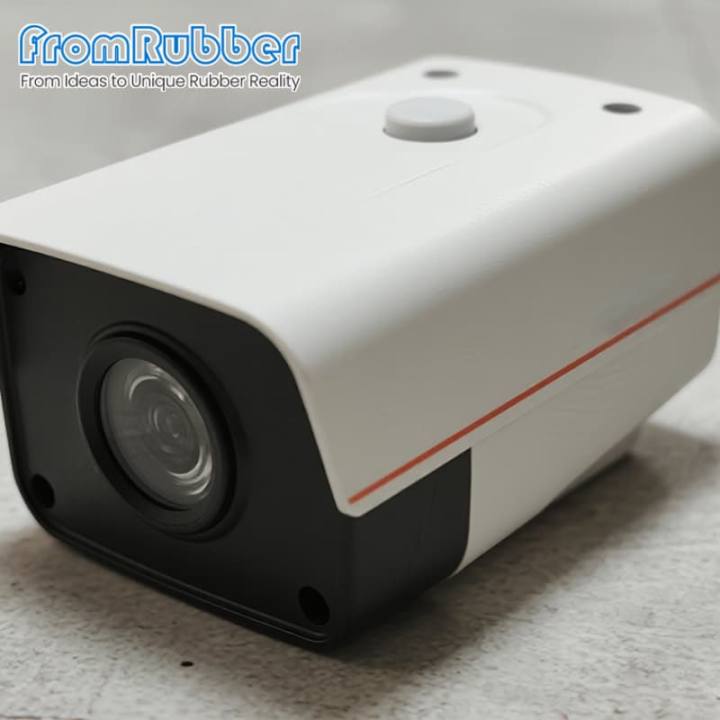
The project started with returns from the previous generation: water in the lens area after heavy rain, yellowing of the front cover after one summer, and a lid that warped when the internal electronics ran warm in direct sun. Each symptom pointed at a different part of the design, and none of them at the resin alone.
The response was to write the failure list into the specification with a test for each item: an IP67 immersion and jet sequence, a UV exposure with a colour measurement, and a thermal cycle from -30 °C to +60 °C with the electronics running. That list later became the validation plan, which is why the project could claim a specific life instead of a general durability statement.
Material selection with the coating decision removed
A painted housing would have solved the UV problem and added a process, a cure, a reject mode and a colour-match argument on every batch. The alternative was a UV-stabilised ABS with a moulded matte texture, which holds appearance without a coating and hides handling marks in the field.
The thermal requirement set the wall sections. ABS at 60 °C ambient with internal dissipation needed thicker sections around the electronics and a rib layout that carries load away from the lid. That is a design answer to a material limit, and it cost less than moving to PC/ABS for the whole housing.
- UV-stabilised grade — removes the paint line and its rejects.
- Matte texture — hides scratches and slows visible chalking.
- Local thickening — cheaper than upgrading the whole part to a higher-grade resin.
Sealing stack and what each layer does
| Layer | Function | Failure if omitted |
|---|---|---|
| Cable gland with a compressible insert | Seals the cable entry against jet and immersion | Water tracks along the cable into the cavity |
| Moulded gasket groove with a silicone gasket | Holds the gasket in place during assembly | Gasket shifts, lid leaks at one corner |
| Lid screws with a defined torque and sequence | Applies even compression around the perimeter | One side under-compressed, leak under thermal cycling |
| Breathable vent membrane | Equalises pressure without letting water in | Pressure-driven ingress on cool-down |
| Drain path at the base | Carries any condensate away from the electronics | Standing water inside the housing |
Where the 20 percent came from
The saving was not a material substitution. It came from four changes: a gate position that removed a cosmetic flow mark and with it a polishing operation; wall sections reduced from 3 to 2.4 millimetres in non-structural areas, which shortened the cycle; a moulded gasket groove that eliminated a manual gasket-fitting step; and a revised lid that used two screws instead of four without losing compression uniformity.
Each change was validated before it was adopted. The thinner wall was checked for stiffness under the drop test, the two-screw lid was checked with pressure-sensitive film to confirm the compression pattern, and the new gate was checked for weld-line position relative to the gasket land. Savings that are not validated this way tend to reappear as field failures.
How a weatherproof housing programme is quoted and run
For an outdoor enclosure the validation plan is part of the deliverable, because the IP claim depends on it.
Inputs
Electronics layout, heat load, cable entries, mounting, climate and the IP target.
Design
Sealing stack, wall sections, gasket groove, vent and drain path, reviewed before tooling.
Validation
IP67 jet and immersion, thermal cycling with the electronics running, and UV exposure with colour measurement.
Volume and cost
Cavity count, cycle estimate, assembly steps removed and the resulting unit cost.
From prototype to production on an outdoor housing
The first moulded samples exposed two issues that a render could not: a weld line running across the gasket land on the hinge side, and a lid that needed more force than the assembly operator could apply comfortably. Both were corrected before the production tool was cut, which is the entire argument for a prototype or bridge step on an outdoor enclosure.
The validation then ran on production parts, not on the prototype. IP67 jet and immersion, a thermal cycle with the electronics powered, and a UV exposure with colour measurement — each test on parts from the same cavity set that would ship. That sequence is what turns a design intention into a claim the sales team can repeat without hedging.
Questions about outdoor housings
Is ABS suitable for ten years outdoors?
A UV-stabilised ABS with a matte texture can hold appearance for a long service life in a temperate climate. In intense sun or coastal salt, PC/ABS or a coated grade is the safer specification.
Does IP67 mean it can be submerged permanently?
No. IP67 covers temporary immersion under defined conditions. A permanently submerged product needs a different sealing philosophy and a pressure test at depth.
Why add a vent to a sealed housing?
Temperature swings create pressure differences that pull water past seals. A breathable membrane equalises pressure while blocking liquid water, which reduces the load on every other seal.
Can the housing be opened for service?
Yes, if the gasket is retained in a groove and the screws have a defined torque and sequence. A gasket that relies on adhesion cannot be reused after the first service.
Send the electronics layout and the climate
FromRubber designs and moulds outdoor ABS and PC/ABS housings in Dongguan, with the sealing stack and validation plan quoted alongside the tool. Send the board layout, the heat load, the cable entries and the installation climate; we will propose a housing and a test sequence that supports the IP rating you intend to claim.
Request an outdoor housing reviewRelated reading: choosing between ABS and other enclosure grades and custom IP65 plastic enclosures.