High-Temperature Compression Set in Steering Wheel Silicone Keypads: Controlling Rebound Loss After 72 Hours at 100°C
- Share
- publisher
- FromRubber
- Issue Time
- Oct 5,2026
Summary
Steering-wheel buttons rarely fail loudly. They return a fraction slower each summer until the tactile character is gone, while a hardness reading still passes. This article separates compression set, hardness change, rebound loss and permanent deformation, and puts the 72-hour test at 100°C inside a keypad-level programme with fixed acceptance numbers.
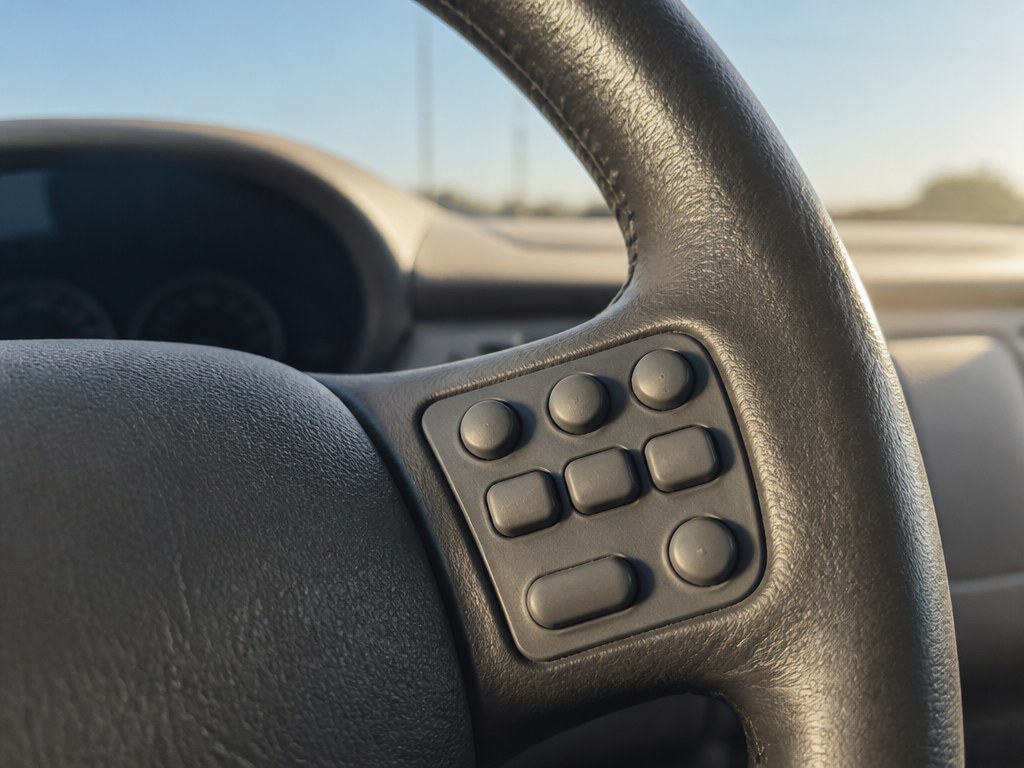
Steering-wheel buttons do not fail loudly. They start returning a fraction of a second slower, then a little slower again, until the driver notices that the volume key needs a firmer push than the one next to it. Nothing has cracked and nothing has discoloured, the part still passes a hardness check, and yet the tactile character that the vehicle team spent months tuning has quietly disappeared — a few months of summer parking did what a year of laboratory testing did not.
What compression set really means on a keypad
Compression set is what is left behind when you squash an elastomer, hold it, and let go. Perfectly elastic behaviour would return the part to its original dimensions; real materials return most of the way and keep a small permanent deformation. On a steering-wheel keypad that permanent deformation is not a theoretical property, because the key sits under load for its entire life. The housing compresses the flange, the return leg rests against a stop, and the key wall holds a resting position. Any of those interfaces can convert a small compression set into a permanent loss of travel.
Four things get mixed up in these discussions, and separating them makes the investigation much faster. They are related, but they are measured differently and they respond to different fixes:
| Property | What it is | How it is measured | Does it predict complaints? |
|---|---|---|---|
| Compression set | Residual deformation after a defined compression at a defined temperature and time | ASTM D395 or ISO 815-1, at a stated compression strain and dwell | Yes — one of the two strongest predictors |
| Hardness change | A shift in the compound’s resistance to indentation | Shore A or IRHD on a defined area, before and after ageing | Partly — a screening check, not a pass/fail criterion |
| Rebound loss | A reduction in the speed and completeness of recovery after release | Return-time and recovery measurement against a defined pre-load | Yes — it is the customer-visible symptom |
| Permanent deformation | The visible geometric result of the three above acting together | Dimensional inspection against reference photographs | Yes — this is what the driver notices |
Where the keypad sits in the product determines which of these governs the complaint. A control panel that a finger only touches while powered may never accumulate enough dwell time for compression set to matter, while a steering-wheel key spends its whole life held at a pre-load. That is why automotive silicone keypads and instrumentation keypads can pass the same material test and still fail differently in the field.
Why 100 °C ageing eats rebound
The compound, not just the grade name
Elevated temperature accelerates everything that happens slowly at room temperature. In a silicone compound those slow processes include further crosslinking, breakdown of the polymer network, and reactions involving residual species. Published work on heat-aged silicone rubber describes a pattern rather than a single trend: Mwafy and Gaafar (Polymer Bulletin 80, 2023) aged a silica-filled silicone compound in air for up to 70 days and found hardness rising overall but passing through two distinct minima — at 14 days and again at 50 days — with tensile strength dropping at the same two points and SEM showing cracks and voids there. Their interpretation is that new crosslinks form early, partially degrade, then partly recover; thermal stability fell at both degradation points. The practical reading for a keypad programme is that ageing behaviour is not a smooth curve, which is why “what happened at 24 hours” does not predict “what happens at 72 hours”.
Curing and post-curing
A compound that is under-cured will continue to change after the part is moulded, and some of that change happens in service at elevated temperature. Post-curing is a controlled way to complete the reaction before the part ships, and it is genuinely useful for improving long-term elastic recovery and reducing volatile content.
It is not a universal fix. Post-curing adds a process step and a cycle time, it can affect pigments and printed legends, and it cannot compensate for a formulation that is simply not suited to the operating temperature. Post-curing is best treated as one variable in the cure profile — alongside temperature, time and pressure — rather than as the answer to every rebound problem.
Geometry decides how much of the material behaviour reaches the driver
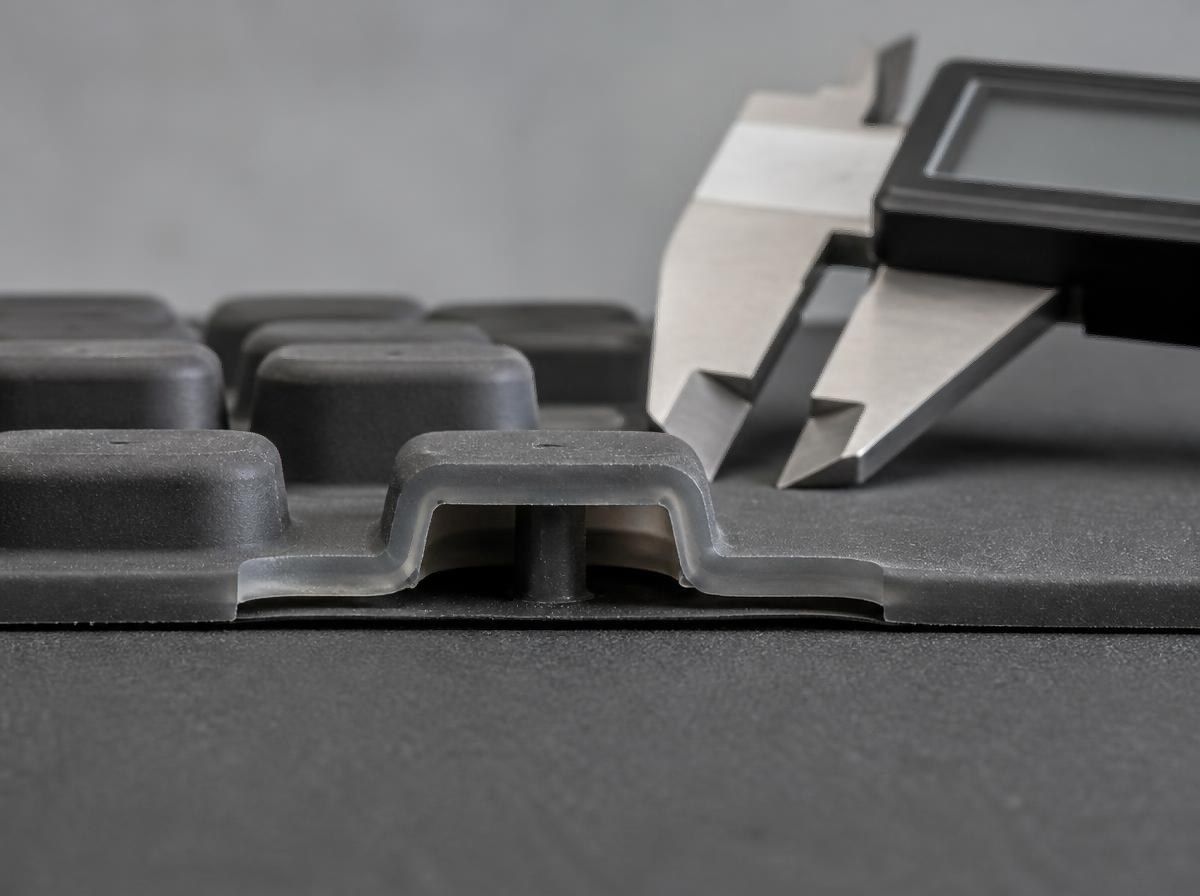
The membrane thickness, the return-leg geometry, how far the key wall is compressed and where local stress concentrates all determine how a given compound change translates into a feel change. A thin membrane is more sensitive to stiffening than a thick one; a long return leg with poor support is more likely to take permanent set than a short, well-anchored one. Two keypads moulded from the same batch in different tools can age very differently, purely on geometry. That is the point at which a custom silicone rubber mould becomes a design decision rather than a production detail: the wall and return-leg section carried into the tool is what determines whether a compound change is felt at all.
Why a hardness reading after ageing is not enough
Hardness after ageing is popular because it is quick, and it is genuinely useful as a screening check. It is not sufficient, because a keypad can hold similar Shore A values before and after ageing while its tactile behaviour moves clearly outside the acceptable window. The four properties that describe what the driver feels are hardness, compression set, actuation force and key travel — and of these, compression set and force are the ones that predict complaints. Measuring on raw material buttons rather than on the finished keypad adds a second layer of unreliability, because the moulded geometry is where the strain concentrates.
A 72-hour at 100 °C heat-ageing sequence
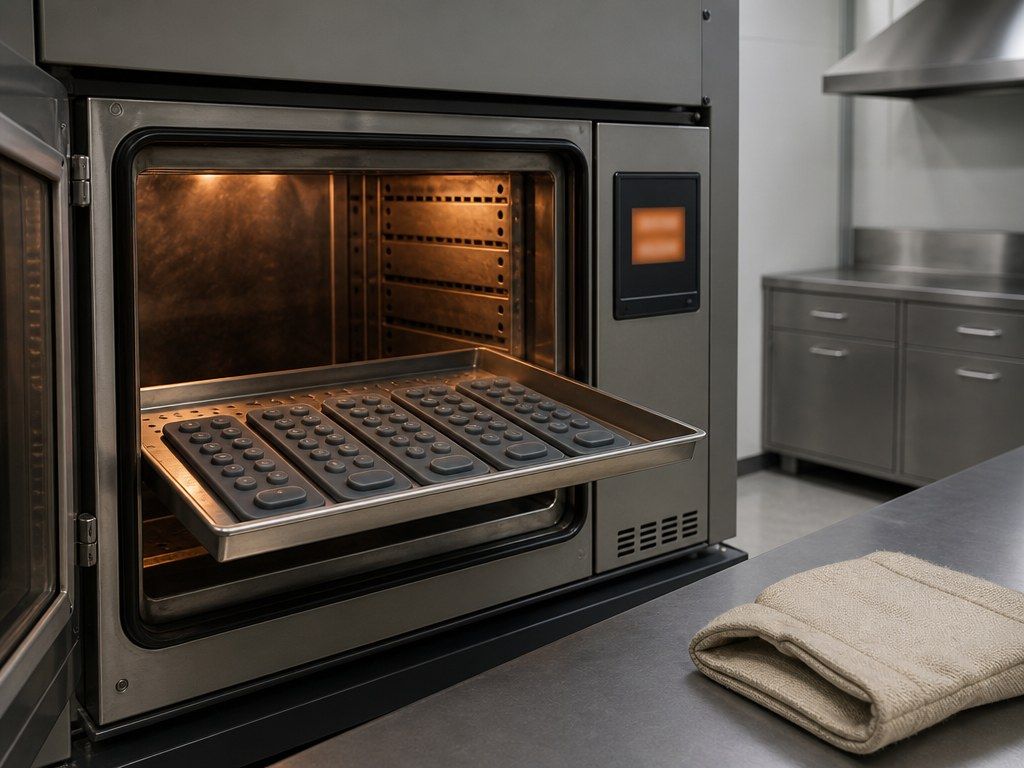
The value of this test is entirely in the acceptance criteria. Two recognised standards cover the measurement itself: ASTM D395-18 gives three methods — constant force in air, constant deflection in air (Method B, the default unless a specification states otherwise, and not suitable above 90 IRHD), and constant deflection considering material hardness. ISO 815-1:2019 gives the equivalent determination at ambient or elevated temperatures for rubber from 10 to 95 IRHD, normally at 25 % compression strain, stepping down to 15 % and 10 % for nominal hardness of 80 IRHD and above. ISO 815-1:2019 also draws a line worth copying into your own programme: short tests of roughly 24 h are treated as a measure of state of cure and compound classification, while tests of the order of 1000 h are what account for ageing and predict service performance. A 72 h test sits between those two purposes — long enough to shift the compound, short enough that it still cannot stand in for a service-life prediction. That is why the acceptance numbers have to come from your own duty cycle rather than from the standard. The sequence below puts the standard measurement into a keypad-level programme:
- Inspect the new keypad and record reference photographs of each key.
- Measure initial hardness on a defined flat area, consistently across samples.
- Measure actuation force and capture the full force–displacement curve for several keys.
- Record key travel at the rated force, and record return behaviour against a defined pre-load.
- Record the as-assembled compression — how much the housing squeezes the flange and how far the return leg is pre-loaded.
- Expose the samples to the ageing condition, keeping the oven loading and airflow the same for every sample.
- Cool the samples under defined conditions. Cooling rate affects the measured result; an uncontrolled cool-down is a hidden variable.
- Repeat hardness, force, travel and return measurements on the same keys, in the same order.
- Inspect for permanent deformation and compare against the reference photographs.
- Compare before and after as a set, and judge against the acceptance numbers written before the test started.
Troubleshooting
| Symptom | Probable cause | Recommended check |
|---|---|---|
| Slow rebound after ageing | Material ageing and incomplete cure | Heat-ageing comparison against a post-cured reference part |
| Visible permanent deformation | High compression set at the interface | Compression-set measurement at the as-assembled compression |
| Higher actuation force | Compound stiffening plus geometry change | Force measurement on the same keys before and after |
| Uneven rebound across the panel | Mould or thickness variation | Dimensional inspection of membrane thickness key by key |
| One area collapses | Local over-compression at the housing | Housing interface and flange compression inspection |
Controlling rebound loss
Select the compound against the real duty cycle
Choose the grade against the actual maximum in-service temperature and how long the part is held there, not against a generic “high temperature” description. A steering-wheel part that sees 80 °C for an hour each afternoon is a different requirement from one that sees 100 °C for a week in a validation oven.
Control hardness and geometry together
Raising hardness to fight set makes the key stiffer, which changes the force the driver has to apply. Softening the compound to restore the force reduces the key’s resistance to compression. Neither move works in isolation. The practical approach is to fix the force window and the travel window first, then treat hardness, membrane thickness and return-leg section as a group that is adjusted together and re-measured as a group.
Control the cure profile
Fix cure time, temperature and pressure as specified parameters with a recorded window, and treat post-curing as a defined step where it is used. Batch-to-batch drift in the cure profile shows up months later as inconsistent rebound, and by then the moulding records are the only evidence left.
Control assembly compression
This is the most under-specified part of most steering-wheel keypad designs. Define the flange compression as a window, specify the mating surface flatness, and check the tolerance stack at the extremes rather than the nominal. A design that relies on nominal tolerance to avoid pre-load will produce a small fraction of units that are over-compressed, and those are the units that generate warranty claims.
Validate the finished part
Test moulded production-intent samples, at the as-assembled compression, with the acceptance numbers fixed in advance. Flat material coupons do not reproduce key-wall strain or flange compression, and they will happily pass a programme that the finished part fails.
Material, design or assembly? One diagnostic order
When a rebound problem arrives, the expensive mistake is to change the compound first. Work through the three layers in order:
- Assembly first — because it is the cheapest to check and the easiest to get wrong. Confirm the actual compression on a returned part. If the flange is squeezed beyond the design window, the material is not the problem.
- Design second — measure membrane thickness and return-leg geometry on the returned part against the drawing. Uneven rebound across a panel is usually a geometry or mould signal, not a compound one.
- Material third — only then compare compounds with a controlled ageing test, keeping geometry constant.
Specification checklist for automotive silicone keypads
- Maximum operating temperature and the longest continuous dwell.
- Heat-ageing test temperature, duration and cool-down condition.
- Hardness range measured on a defined area of the part, and the unit it is expressed in (Shore A or IRHD).
- Which compression-set method is being used — ASTM D395 Method B, or ISO 815-1 — because the two are not interchangeable without a stated correlation.
- Compression strain and dwell used for the set measurement, and the cool-down condition.
- Actuation-force window and key-travel window, before and after ageing.
- Rebound or recovery requirement, with the pre-load at which it is measured.
- Compression-set limit measured at the as-assembled compression.
- Expected actuation cycles over the vehicle life.
- Flange compression window, mating surface flatness and tolerance stack check.
- Surface and legend requirements, including ageing appearance limits.
How this is handled in production
Steering-wheel keypad programmes go wrong most often at the boundary between the silicone part and the housing. On heat-aged automotive keypad projects at FromRubber the working method has been to obtain the as-assembled compression from the customer, reproduce it in the ageing fixture, and measure force and recovery on the same keys before and after — which makes an assembly-driven problem visible before anyone starts changing compounds. Customers can send the compression window and force window they are working to and we will quote against them, which is the fastest way to find out whether a set limit is realistic for the geometry you actually have.
FromRubber moulds custom silicone rubber parts: keypad panels, gaskets, seals and technical mouldings. We do not manufacture the steering wheels, control modules or vehicle interiors our parts are fitted into. What we can do is mould to the stated compression window, run heat-ageing on the finished geometry, and report the before-and-after comparison rather than a single set of numbers. Production-intent samples and the ageing fixture are described in more detail under mould making, and the keypad formats we build are listed under custom silicone rubber keypads.
What to take away
Long-term rebound on a steering-wheel silicone keypad is decided by four things at once: the compound’s behaviour at the service temperature, the completeness of the cure, the geometry of the membrane and return structures, and the compression the housing applies. A 72-hour test at 100 °C is a useful tool when the acceptance criteria — force window, travel window, recovery and compression-set limit — are written down before the samples go in, and almost useless when they are not. Start the diagnosis at the assembly interface, not at the material certificate.
References
- ASTM D395-18, Standard Test Methods for Rubber Property — Compression Set — Method A (constant force in air), Method B (constant deflection in air, the default unless otherwise specified, not suitable above 90 IRHD), Method C (constant deflection considering material hardness).
- ISO 815-1:2019, Rubber, vulcanized or thermoplastic — Determination of compression set — Part 1: At ambient or elevated temperatures — edition 3, published 2019-11, confirmed still current in 2025. Covers 10 to 95 IRHD, normally at 25 % compression strain, reduced to 15 % and 10 % for nominal hardness of 80 IRHD and above. Distinguishes short tests of about 24 h (state of cure, compound classification) from tests of the order of 1000 h (ageing and service-performance prediction).
- ISO 815-2:2019, Rubber, vulcanized or thermoplastic — Determination of compression set — Part 2: At low temperatures — the companion low-temperature method, listed here for completeness. It does not cover the 100 °C elevated-temperature condition discussed above; use ISO 815-1 for that.
- Mwafy, E. A. and Gaafar, M. S., “Dynamic mechanical characteristics of aged silicone rubber blend”, Polymer Bulletin 80, 9015–9032 (2023) — DOI 10.1007/s00289-022-04488-5. Heat ageing of a silica-filled silicone compound in air for up to 70 days; hardness and tensile-strength minima at 14 and 50 days.
Related reading: Silicone keypad technology articles including selecting the right tactile force for control-panel silicone buttons and PCB alignment issues before tooling. If you have a heat-ageing requirement and an assembly compression window to work to, send both to nani@fromrubber.com or karl@fromrubber.com, or reach us on WeChat / WhatsApp at +86 18676210913. FromRubber (Dongguan Bohao Electronic Technology Co., Ltd.) — custom silicone rubber parts, Dongguan, China.