How to Design a Silicone Sunglasses Case Without Making It Too Bulky?
- Share
- publisher
- FromRubber
- Issue Time
- Oct 26,2026
Summary
Most bulky silicone sunglasses cases are not a styling problem. They are four ordinary decisions - wall thickness, internal clearance, opening design and compound hardness - made separately and never added together. A practical guide to keeping a custom silicone sunglasses case slim without giving up protection.
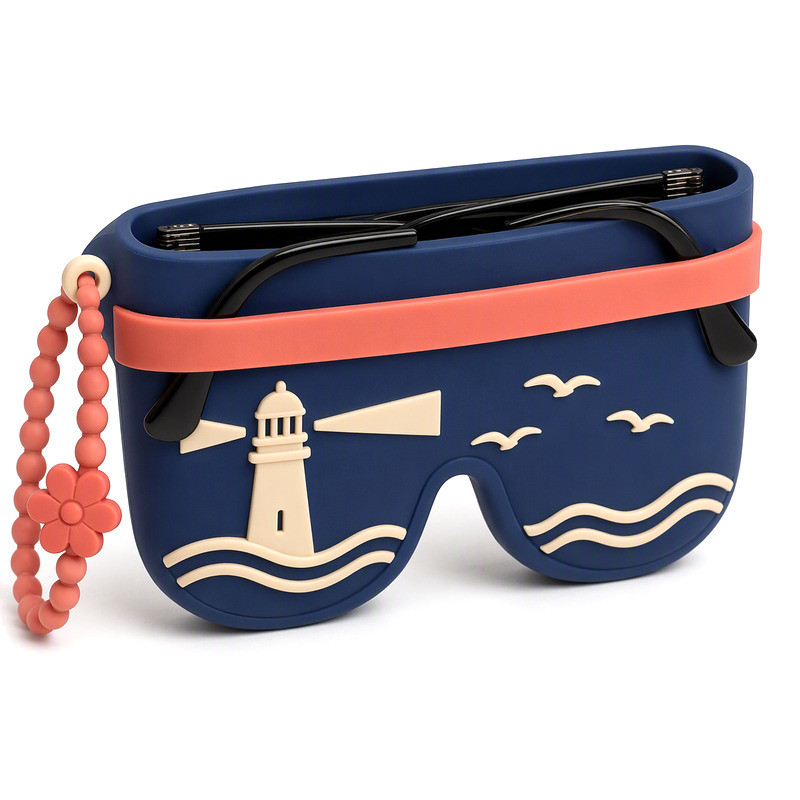
A silicone sunglasses case can look slim in a render and still come back from the tool shop feeling closer to a pencil box. By then the mold is cut. The extra volume almost never comes from one bad decision. It comes from four ordinary ones - wall thickness, internal clearance, opening design, and compound hardness - each made in a different meeting, none of them added together.
What Makes a Silicone Sunglasses Case Feel Too Bulky?
Bulk is a ratio problem before it is a styling problem. The same 7 mm wall reads as protective on a 150 mm frame and as a brick on a 132 mm frame. Buyers usually notice it by weight, or by the way the case sits in a tote bag, long before anyone measures it against the drawing.
Thick Walls Can Add More Volume Than the Product Needs
A silicone wall is not a structural member in the way a polycarbonate shell is. Going from 2.5 mm to 4 mm does not make the case four times stronger. It mainly adds mass, slows the cure in that section, and pushes the outer profile outward on every surface at once - front panel, back panel and rim. A 1.5 mm increase applied all round can add 3 to 4 mm to the finished stack.
The more useful question is not "how thick should the wall be" but "which zones actually carry load". On a folded-frame case that is the bridge, the temple entry, and the rim the frame presses against. The lens area carries almost nothing and can usually be the thinnest part of the part.
This is the same failure mode that shows up later as uneven wall sections in production: a design that is thick where it did not need to be often ends up thin where it did.
Extra Space Inside the Case Can Make the Whole Design Larger
Internal clearance is the other half of the equation, and it is where most oversizing starts. A case specified around "a typical wayfarer" usually ends up sized for the largest wayfarer anyone could find in the office, plus a few millimetres of slack "for safety". That slack is then wrapped in a wall, so every millimetre of internal air becomes two or three millimetres of external volume.
Sunglasses vary more than buyers expect. Lens width across a normal commercial range commonly runs from roughly 48 mm to 62 mm, temple length from about 135 mm to 150 mm, and folded thickness depends heavily on hinge type and front curvature. If the brief does not name a range, the designer will protect the entire range, and the smallest frame in that range pays for it.
There is a second layer to this: the molded part itself moves inside its tolerance band. ISO 3302-1:2014 sets dimensional tolerance classes for moulded solid rubber products, and the class you agree on decides how much a nominal 2 mm gap can actually vary from part to part (ISO 3302-1:2014). A design that relies on a 2 mm gap holding exactly 2 mm will be over-built by whoever has to hold that number in production.
A Wide Opening or Oversized Closure Can Change the Overall Profile
The opening is a structural decision wearing the costume of a convenience feature. A sleeve with a full-length side slot can be slimmer than a shell with a lid, because a lid needs a lip, a hinge land, and enough wall to hold a snap or a band. On a 20 mm tall profile, that lip alone can eat 3 mm.
The trade-off is real: a wider mouth is easier to use one-handed, and an easier mouth is usually a bulkier closed shape. What is not real is the assumption that convenience requires a rolled lip. A chamfer at the mouth, or a short flare, solves insertion at a fraction of the volume that a rolled edge costs.
How Much Silicone Does the Case Actually Need?
Start With the Sunglasses Dimensions, Not the Outer Case
Before anyone draws an outer profile, collect the frame. Lens width, total frame width, folded height at the bridge, temple thickness at the hinge, and the front base curve. If a range is intended, get three physical frames: the smallest, the largest, and the most awkward one - usually a thick acetate frame with a sprung hinge.
Clearance should be enough to let a thumb slide the frame in without pressing on the lenses, and no more. That is a functional statement, not a number, and it is the right level to brief at. The number comes from the frame dimensions, the wall you can mold, and the tolerance class you can hold.
Use Different Wall Thicknesses Where the Design Allows
Variable wall thickness is normal in silicone, but it is not free. During compression molding, compound flows from thick sections toward thin ones. A sharp step can starve the thin side, and cure time is set by the thickest section, so one generous rib can slow the whole cycle.
The practical rules are unglamorous. Taper the transition over about three times the thickness difference. Avoid a step that a knife edge has to fill. Keep the thinnest section thick enough to survive demolding without tearing at the rim.
This is also where a compact design becomes manufacturable or not. A 1.2 mm panel with a 4 mm boss next to it will mold, but the transition has to be designed rather than left to the toolmaker's judgement.
Choose Silicone Hardness Based on the Intended Case Structure
Hardness decides whether the case behaves like a sock or like a shell, and it is the number most often copied from a previous project. A soft compound collapses and relies on the sunglasses to hold the shape. A firmer compound keeps a curve on its own but fights you every time you insert a frame.
It is worth being precise about what the number means. Shore A hardness is a material property measured on a cured test piece under ISO 48-4:2018 or ASTM D2240, not a promise about how a finished 2 mm wall will feel in the hand (ISO 48-4:2018). Two compounds with the same nominal hardness can behave differently once wall thickness and geometry are in play - which is why hardness alone is a poor predictor of case performance.
Which Case Structures Help Keep the Design Compact?
A Simple Sleeve May Work Better Than a Fully Enclosed Shell
The two structures solve different problems. A sleeve covers the front and the rim and leaves one side open; it is thinner, lighter, and cheaper to tool because there is no lid, hinge or closure to build. A full shell encloses the frame and protects it from being crushed inside a bag, but it pays for that protection in wall, in lip and in a second molding step.
If the product travels in a handbag next to keys, the shell argument is strong. If it hangs from a strap or lives in a car door pocket, the sleeve usually wins, and the sunglasses are no worse off.
Keep Ribs, Raised Edges, and Decorative Features Functional
Every raised feature adds local thickness. A 1.2 mm relief adds 1.2 mm where it sits, plus draft on both flanks, and the mold has to cut that shape into steel. That is a fair price for a feature that grips, locates the frame, or reads as a brand at arm's length. It is a poor price for texture that only exists because the render looked empty.
A useful test for each element: does it grip, does it locate, does it read at 300 mm? If it fails all three, consider debossing it instead of raising it. Engraved decoration removes material rather than adding it, and on a compact case that difference shows up in the pocket.
Check Whether the Opening Can Be Simplified
There are only a few opening families worth comparing: a full-length side slot, a curved mouth that follows the frame, a narrow slit relying on stretch, and a tab or band that closes the end. Each one changes insertion force, retention and the closed silhouette.
Evaluate the whole interaction rather than the closed dimensions. A case that measures 6 mm thinner but needs two hands and a table to load will be returned by the customer, and the drawing will not show that.
What Should Be Checked Before Approving the First Sample?
Test the Fit With the Actual Sunglasses
Not a dimensional sample - the actual product, in every frame size you intend to sell. Insert and remove it ten times. Watch where the frame touches the case, whether the temples catch, and whether the lens presses against the front panel. A case that leaves a fingerprint on the lens is a design fault, not a cleaning problem.
Review the Case in Both Its Open and Closed States
Open, the mouth should not gape or fold back on itself. Closed, the sides should stay parallel rather than bulging at the middle. Compare the sample against the agreed drawing with calipers at three points, not by eye, and note where the part sits inside its tolerance band.
Check Whether the Compact Design Can Be Manufactured Consistently
A thin, tight design has less room for process variation, so the tooling has to be reviewed earlier than usual. Look at parting line placement, undercuts that need a split or a manual demold, and whether the mouth can be stripped off the core without stretching the rim permanently. Parting line design and shrinkage allowance are the two places where a slim concept usually needs adjusting before steel is cut.
What Should You Send a Manufacturer for a More Accurate Design Review?
You do not need a finished CAD model to get a useful opinion. A short package is enough for a manufacturer to tell you where the volume is going:
- Frame dimensions, or one physical frame per size you plan to cover.
- Target outer dimensions and the profile you want to see in a pocket.
- Wall thickness intent, or the zones that must be thicker.
- Hardness preference, or a description of the feel you want.
- Opening concept, even as a rough sketch.
- Protection level and where the product will be carried.
- Logo placement, colour split and texture requirements.
- Estimated quantity and expected reorder pattern.
What usually moves a project forward fastest is the physical frame. A 3D file tells a toolmaker the shape; a frame in hand tells everyone whether the case will feel right.
Conclusion
A slim silicone sunglasses case is not a case with thinner walls. It is a case where the wall thickness follows the load, the internal clearance follows a named frame range, the opening is the simplest one that still works, and the hardness matches the structure rather than the previous project. Get those four aligned and the outer dimensions take care of themselves.
FromRubber has been molding custom silicone parts in Dongguan since 2010, with tool making, molding and finishing under one roof, which makes it possible to review a compact concept against real tooling constraints before a mold is cut. If you are working on a sunglasses case and want a second opinion on where the volume is coming from, send the frame dimensions or a sample to our engineering team - or write to nani@fromrubber.com.
FromRubber is the brand of Dongguan Bohao Electronic Technology Co., Ltd., a custom silicone manufacturer based in Dongguan, China, molding since 2010. The company holds IATF 16949:2016, ISO 9001:2015 and ISO 14001:2015 certification and runs two plants with 32 compression molding presses.
FAQ
How thick should a silicone sunglasses case be?
There is no universal number, and any supplier who quotes one without seeing your frame is guessing. Thickness should be set per zone: enough at the bridge and temple entry to resist collapsing, thinner across the lens area where almost no load passes through. The wall you can mold consistently also depends on hardness, geometry and the tolerance class you agree.
Can a soft silicone sunglasses sleeve protect different frame sizes?
It can cover a range, but not an unlimited one. Define the smallest and largest frame by lens width, total width and folded thickness, then design the clearance around that range. A sleeve sized for a 62 mm lens will feel loose on a 48 mm frame, and loose is where lenses get scratched.
Does softer silicone always make a sunglasses case more compact?
No. Softer compound lets you use a thinner wall in some areas, but it also collapses under its own weight, so a shaped case may need extra structure to keep its profile. Hardness and geometry have to be chosen together.
Can wall thickness vary within a custom silicone case?
Yes, and it usually should. The constraint is process, not principle: transitions need to be gradual enough for compound to flow, and cure time follows the thickest section, so a heavy local rib can slow the cycle and raise cost.
What information does a manufacturer need to review a compact case design?
A frame sample or accurate frame dimensions, the outer profile you want, the opening concept, and any hardness or colour requirements. A rough sketch plus one physical frame is usually more useful than a detailed drawing with no reference product.
Sources
ISO 3302-1:2014, Rubber - Tolerances for products - Part 1: Dimensional tolerances. iso.org/standard/62492.html
ISO 48-4:2018, Rubber, vulcanized or thermoplastic - Determination of hardness - Part 4: Indentation hardness by durometer method (Shore hardness). iso.org/standard/74969.html