Multi‑Color Silicone Keypad Misalignment? Overmolding Challenges & Solutions
- Share
- publisher
- Suey
- Issue Time
- Aug 5,2026
Summary
Fixing colour misalignment on a multi-color silicone keypad: why 0.1mm of first-shot movement is visible, how locating pins, interlocking geometry, vision transfer and 1.5-3% shrinkage compensation hold a boundary, and the case that moved from 0.3mm to under 0.05mm.
Colour misalignment on a multi-color silicone keypad is a locating problem, not a printing problem. In two-shot moulding the first colour is moulded, then the semi-finished part is moved into a second tool — and if it sits even 0.1 mm off, the offset is visible at the colour boundary before any legend is applied.
The reliable route to a sharp boundary is mechanical, not operator skill: locating pins and matching holes cut into both the tool and the first-shot part, automated transfer with vision alignment for anything tighter than ±0.1 mm, gate placement that sends second-shot material away from the boundary, and shrinkage compensation for the 1.5–3.0% the first shot loses after demoulding.
Where a multi-color silicone keypad goes out of register
Four variables decide whether the second colour lands where the drawing says it should. They interact, so fixing one in isolation rarely holds a tolerance.
Part positioning
The first-shot part is a flexible solid, not a machined block. Any play in the second-shot cavity translates directly into boundary offset, and 0.1 mm is already visible on a small key.
First-shot shrinkage
Silicone shrinks 1.5–3.0% after moulding. If the second tool is cut to nominal dimensions, the alignment feature itself is undersized by the time the part arrives — a systematic error that repeats on every cycle.
Second-shot injection pressure
High pressure displaces a part that is not firmly clamped. The offset then varies across the panel, which is the signature that separates a pressure problem from a locating problem.
Flash and colour migration
Second-shot material seeps under or around the first-shot edge and bleeds across the boundary. This looks like misalignment but is a clamping and gate issue.
The colour boundary is a moulded interface. Its sharpness is set by locating features and clamp force, not by the artwork.
The fixes that hold a boundary tolerance
| Countermeasure | What it controls | Practical note |
|---|---|---|
| Locating pins and matching holes in both tools | Repeatable part position | Put features outside the visible area; two pins minimum, diagonally opposed |
| Interlocking first-shot geometry | Resistance to displacement under second-shot pressure | A shallow step or tongue on the first shot gives the second shot something to key into |
| Vision-guided automated transfer | Position repeatability below ±0.05 mm | Manual loading is adequate above ±0.1 mm; below that, it is not |
| Gate positioned away from the boundary | Flow-induced displacement and wash-out | Fill the thick region first and let the boundary be the last place material arrives |
| Shrinkage compensation in the second tool | Systematic offset that repeats every cycle | Measure the first shot, not the mould, before cutting steel |
Two of these are design decisions and three are process decisions. In practice, a supplier that has only process answers — "we will be careful" — cannot hold ±0.05 mm on a flexible part.
Case: a 0.3 mm offset on a game controller D-pad
A controller programme specified less than 0.1 mm deviation at the colour boundary between a red and a black section of the D-pad. The first samples came in at 0.3 mm — three times the limit — and the effect was worse than the number suggests: the two colours blended at the edge, and the whole cluster read as poorly made.
Root cause was twofold. The first shot was located by cavity fit alone, with no positive locating feature, and the second tool had been cut to nominal dimensions without compensating for first-shot shrinkage. Clamp pressure was also high enough to push the part slightly off position on the gate side.
The fix added two locating pins with matching holes moulded into the first shot, moved the gate so the boundary filled last, and reduced second-shot pressure. Final parts held under 0.05 mm consistently, inside the design tolerance with margin to spare.
Sharp separation comes from positive location on every cycle, not from a tighter visual inspection at the end of the line.
Specifying a multi-color silicone keypad without ambiguity
Most misalignment disputes start with a drawing that describes colour areas as artwork rather than as moulded geometry. Five items remove that ambiguity:
- Boundary tolerance stated as a number, in millimetres, on the drawing — not as "sharp".
- Which colour is shot first, and where the locating features may sit.
- Pantone references for both colours, plus the acceptable shift after vulcanisation.
- Whether a third colour is moulded or printed; mixing the two on one key changes the tolerance stack.
- Sample quantity for first-article inspection, with the measurement method for boundary offset.
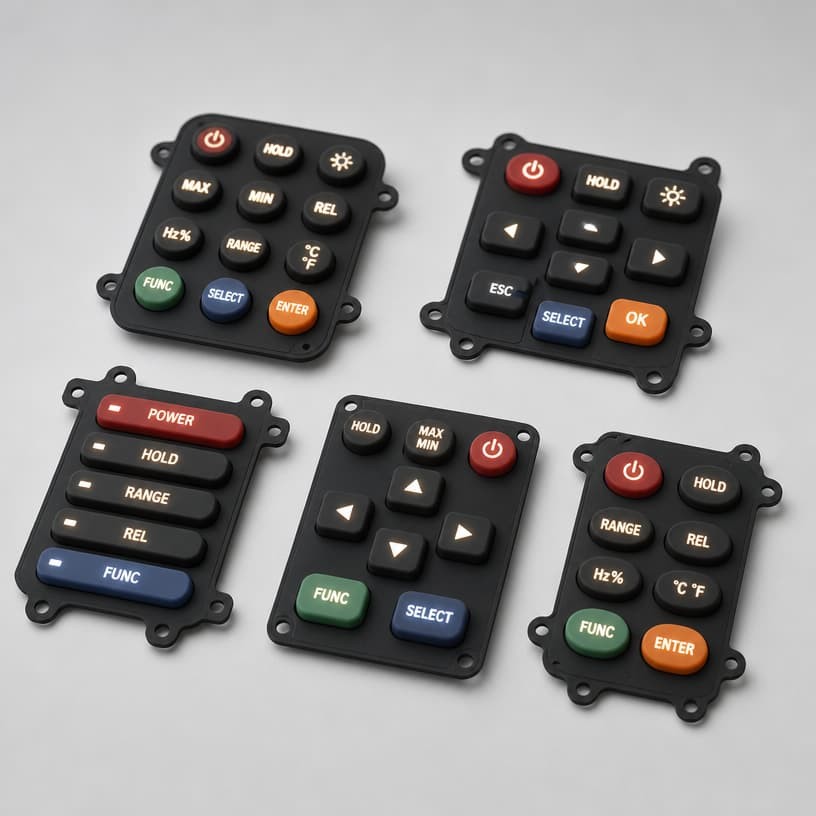
A second moulded colour on function keys is a structural surface, not decoration — which is the case where two-shot earns its tooling cost.
The alternative — sending a reference sample and asking for "the same" — works only when the supplier has the same tools and the same transfer method, which is rarely true.
Two-shot is not always the right answer. Where the second colour sits on a flat, low-wear area, pad printing or laser etching can meet the visual intent at lower tooling cost. Two-shot earns its cost when the second colour is a structural surface that must not wear off.
Questions buyers ask about two-shot colour
What boundary tolerance is realistic?
±0.1 mm is achievable with good locating geometry and manual transfer. Below that — to ±0.05 mm — vision-guided automated transfer is the practical route. Asking for ±0.02 mm on a flexible silicone part is asking for a measurement dispute.
Can existing single-colour tools be converted?
Usually only the first-shot tool survives. The second tool must be new, because it needs locating features and shrinkage compensation that the original never had.
Why does the offset vary across one panel?
That pattern points to second-shot pressure displacing the part rather than to a locating error, which would be uniform. Lower injection pressure and better clamping are the first things to change.
Does colour migration always mean flash?
No, but the two are related. Migration is material crossing the boundary; flash is material escaping the cavity. Both come from insufficient clamping at the boundary and are fixed by the same tool change.
Send the boundary tolerance, not a picture
Share the 2D drawing with the colour boundary dimensioned and the wear requirement stated. We will confirm whether two-shot, pad printing or laser etching meets it, then prove the tolerance on a first article before the production tool is cut.
See multi-colour silicone products and the over-moulding process.