Rubber Overmolding: A Smarter Way to Unite Plastic & Metal
- Share
- publisher
- Suey
- Issue Time
- Jul 3,2025
Summary
How rubber overmolding bonds by chemical adhesion or mechanical interlock, which mechanism suits which substrate, two-shot versus insert moulding, substrate preparation, and how to read a delamination failure.
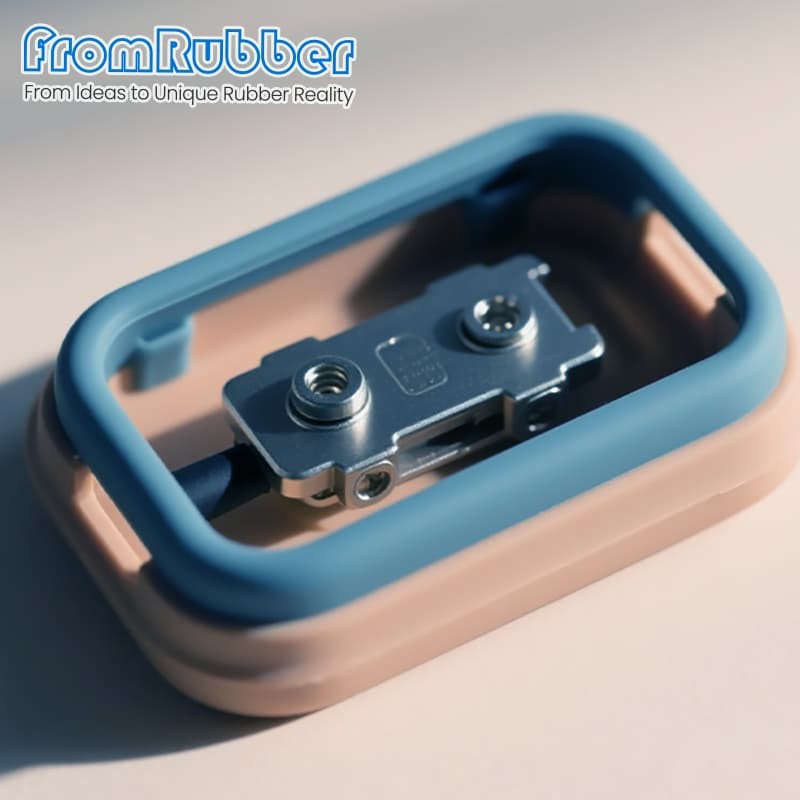
Overmoulding looks like a material decision and is really a bonding decision. The rubber either adheres chemically to the substrate or it is held mechanically by geometry, and a part designed for one will fail if the other is used.
This covers rubber overmolding as a design problem: which mechanism applies, how the substrate has to be prepared, and how a delamination failure is diagnosed before it reaches a customer.
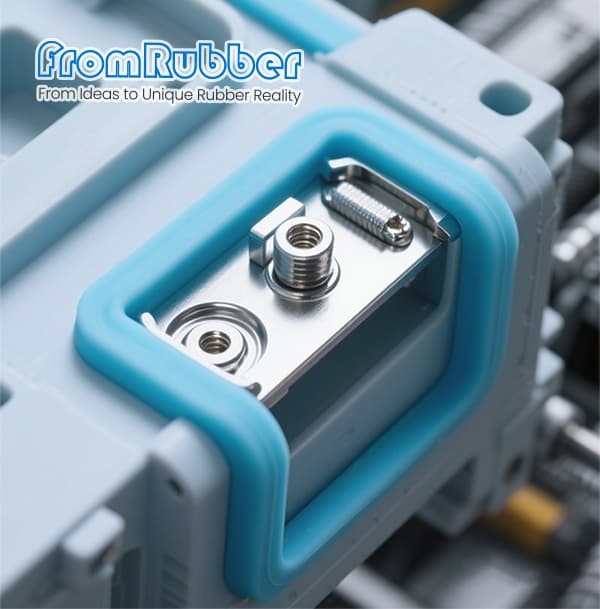
How Does Rubber Overmolding Actually Bond?
The direct answer: by chemical adhesion, by mechanical interlock, or by both. Chemical bonding needs a substrate that the rubber can react with, plus a clean and often primed surface. Mechanical interlock needs holes, undercuts or a textured surface that the rubber flows into and cannot pull out of.
Most production parts use both, because chemical adhesion alone is sensitive to contamination and mechanical interlock alone leaves a path for water along the interface.
Choosing the Mechanism
The first row explains a common disappointment: a beautifully designed overmoulded PP part peels because the material was never going to bond chemically, and no primer makes it reliable.
| Substrate | Realistic mechanism | Note |
|---|---|---|
| Polypropylene | Mechanical interlock | Low surface energy makes adhesion unreliable |
| Polycarbonate, ABS | Chemical with priming | Solvent sensitivity in the primer |
| Nylon | Mechanical, or chemical after conditioning | Moisture content affects the bond |
| Aluminium | Mechanical plus primer | Anodising changes the surface chemistry |
| Steel | Mechanical, often with a knurled or drilled feature | Corrosion protection must survive the process heat |
The Process Choices: Two-Shot or Insert
Two-shot moulding injects the substrate and then the rubber in the same tool, with the part transferred between cavities. Insert moulding loads a pre-made substrate into the tool and moulds rubber around it. Two-shot gives better bond consistency and no handling; insert is more flexible for low volume and for substrates that cannot be injection moulded, such as metal.
The choice affects tooling cost more than unit cost at low volume, and it affects the achievable bond at high volume. Where the part is safety-related, consistency usually justifies two-shot.
Preparing the Substrate
Degreasing, drying and, where needed, priming are not optional steps. Nylon absorbs moisture and must be conditioned before moulding or the bond will be inconsistent between lots. Metal inserts need a clean, oxide-free surface and a design that keeps the primer out of the assembly areas.
Diagnosing a Delamination Failure
Look at where the rubber separated. A clean separation at the interface with a glossy surface means the bond never formed, which points at contamination or the wrong mechanism. A separation that tears through the rubber itself means the bond was stronger than the material, and the design should reduce the peel load rather than improve the adhesion. A separation that starts at an edge and runs inward means water or a solvent entered along the interface.
Each of those three has a different fix, which is why "the rubber came off" is not a useful failure description. Sectioning a sample and looking at the failure surface takes an hour and usually settles the argument.
Where the overmoulded part also has to seal, the interface is a leak path as well as a bond line. Our comparison of silicone and rubber seals covers material selection, and the design constraints of the plastic side are set out in the injection moulding guide.
Starting an Overmoulding Project With a Factory
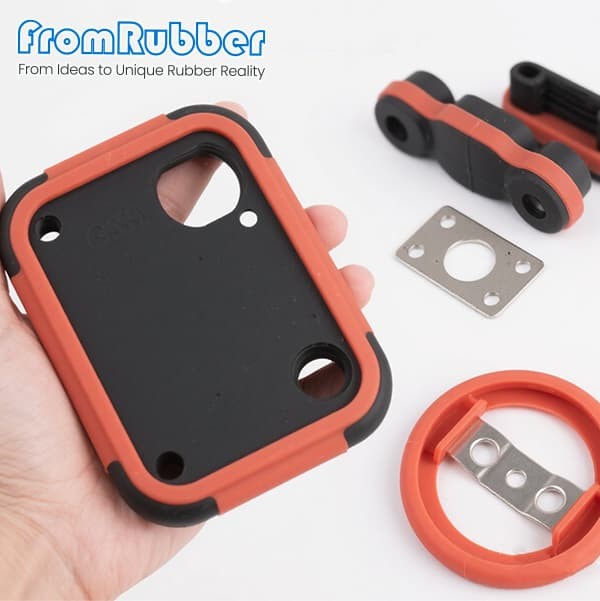
Overmoulding briefs fail for a predictable reason: they describe the rubber and forget the substrate. A workable enquiry names the substrate material and grade, its surface condition, whether it will be supplied as an insert or moulded in the same tool, and the load the bond must carry.
Where the rigid half is also being made, the two parts should be designed together. Our custom plastic enclosure manufacturing page shows how the plastic side is handled when a programme combines both processes.
Frequently Asked Questions
Can silicone be overmoulded onto metal?
Yes, usually with a primer and a mechanical feature. The metal surface must be clean and the primer compatible with the cure system, otherwise the bond forms only where the rubber is trapped.
Why does overmoulded rubber peel at the edge?
The edge is where peel stress concentrates and where cleaning agents first enter. A rolled edge or an undercut that hides the interface removes most of the problem.
Is overmoulding cheaper than assembling two parts?
At volume, usually yes, because it removes labour and a fastening step. At low volume, the tooling often makes assembly cheaper, which is why prototypes are frequently bonded rather than moulded.