Custom Silicone Rubber Products Customization Options and Benefits
- Share
- publisher
- karl
- Issue Time
- Sep 8,2025
Summary
Custom silicone rubber products are quoted three different ways when the RFQ is missing six lines: grade and hardness, colour system, tolerance class, surface, post-processing and inspection. What each omission costs.
Custom moulding / specification - reviewed 11 November 2026
Ask three factories to quote "a custom silicone part" and you will get three numbers that cannot be compared. Nothing is wrong with the factories. The request simply did not contain the six lines that decide how the part is made, and a factory missing those lines has to assume something. The assumptions are where the price difference lives.
Colour is the last of the six, not the first. The earlier five, grade, tolerance, surface, post-processing and inspection, are what turn a shape into a product that can be re-ordered in eighteen months without a second tooling round.
Definitions. Custom silicone rubber products are parts moulded to a customer drawing, where the compound, the tool and the inspection plan are all specific to that part. A tolerance class is a published band of permitted variation for moulded rubber, used instead of writing a tolerance on every dimension. Post-processing covers everything after demoulding: post-cure, printing, laser marking, adhesive backing and assembly.
Programme reference points
- Prototype tool: a 150 x 150 mm plate, single cavity.
- Production tool: a 350 x 350 mm plate, typically 15 to 50 cavities.
- 32 compression presses across two plants in Dongguan.
- IATF 16949, ISO 9001 and ISO 14001 certified processes.
The six lines that make custom silicone rubber products comparable
Grade and hardness
"Silicone" is a family, not a material. A general-purpose 50 Shore A compound and a 70 Shore A high-consistency compound are different products with different moulding behaviour and different data sheets. Write the grade, the hardness with a tolerance of plus or minus 5 Shore A, and the properties that actually matter: tensile strength, elongation, compression set and temperature range.
Colour system
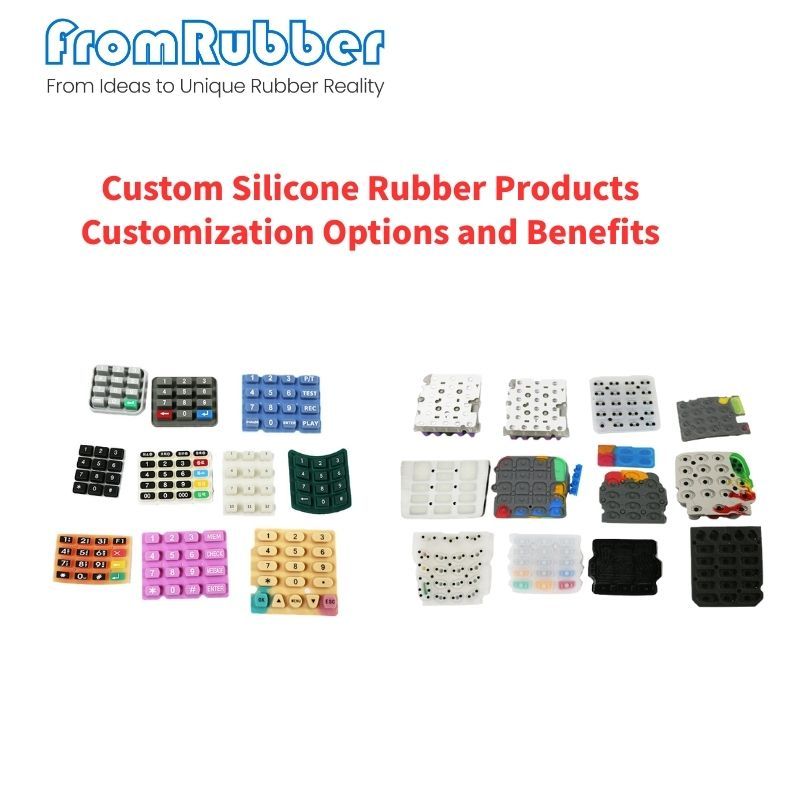
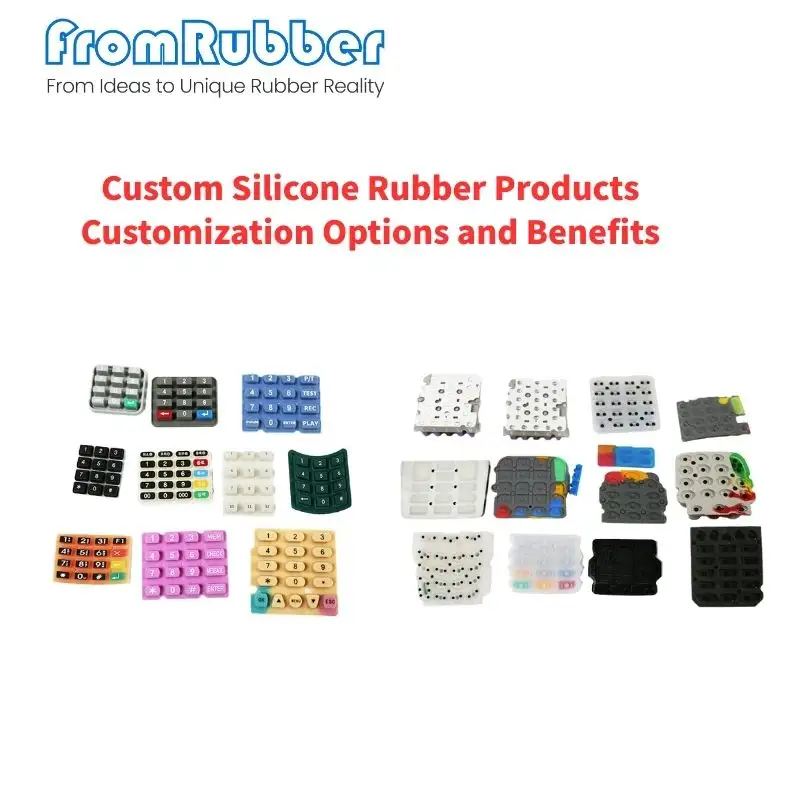
Moulded colour lives inside the part and cannot peel, but the tool is limited to two colours. Printed colour carries up to six plus fine detail, at the cost of an extra process and a print line that has to be positioned against the split. Write the Pantone reference per colour, say which colours are moulded and which are printed, and state where print is not allowed to land.
The remaining four lines
| Line | What to write | Cost of leaving it out |
|---|---|---|
| Tolerance class | A moulded-rubber class such as ISO 3302-1 M as the default, plus the two or three dimensions that carry function | Fit failures at assembly, or a tool inflated by tolerances nobody needed |
| Surface and finish | Gloss or texture reference, acceptable parting-line position, whether visible flash is a rejection | A cosmetic rejection at incoming inspection on a part that works |
| Post-processing | The full route in order: post-cure, print, laser, adhesive, assembly | Adhesion failures, odour in a closed pack, or a second supplier mid-project |
| Inspection and packaging | Pack configuration, AQL level, and the declarations the receiving inspection will ask for | A shipment held at the border or at the customer's dock |
Geometry decides the process before price does
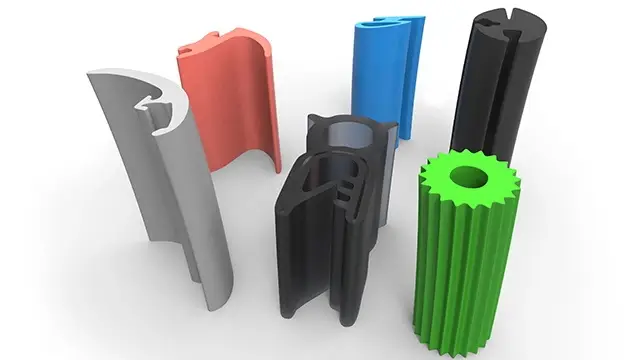
A constant cross-section, a sleeve, a U-channel or a cord, is an extrusion, and extrusion is priced by the metre from a die rather than by the shot from a cavity. The moment the part needs a flange, a closed end, a moulded-in boss or an undercut, it becomes a moulded part and the economics change with the plate size.
Wall thickness has a similar rule
Very thin printed parts and thicker moulded sections do not behave the same way in the tool, and around one millimetre is where flexible parts usually balance feel against mouldability. A section drawing with the wall called out lets a factory say which process you are actually asking for, instead of quoting the one it prefers.
Why a prototype tool earns its cost
A single cavity in a 150 x 150 mm plate proves geometry, hardness and colour before anyone pays for a 350 x 350 mm production tool with 15 to 50 cavities. That is also the point where the six lines get tested rather than assumed: a hardness that moulds well but seals badly is cheap to discover at prototype and expensive to discover after the production tool exists.
Certification matters here because it changes how a change reaches you. A process certified to IATF 16949 carries part-level traceability and a change-notification discipline; a general-purpose process may not. The parts may look identical and behave identically in service, but the paperwork that protects a re-order is not the same.
Commissioning a part
Send the drawing with the six lines filled in, and the answer becomes a price you can compare rather than a number you have to negotiate. The custom silicone rubber parts range shows the formats, and the production process overview sets out the tooling and inspection sequence.
What is the single most useful line in a silicone RFQ?
The hardness with a tolerance, plus the two or three dimensions that carry function. Everything else can be discussed; those two decide whether the part works.
Why do quotes for the same drawing differ by 30 percent?
Usually because one factory assumed printed colour and the other assumed moulded colour, or because one included post-cure and inspection and the other did not. The drawing rarely says.
When is extrusion cheaper than moulding?
When the cross-section is constant and the part needs no flange, closed end or undercut. Adding any of those converts the part to moulding, and the price jumps with the plate size.
Capacity, tool sizes and certification scope quoted here describe the manufacturer's stated capability. A specific project should confirm the applicable certificate scope and the tool route in writing.
To get a comparable number, send the drawing and the six lines through the quotation file checklist.