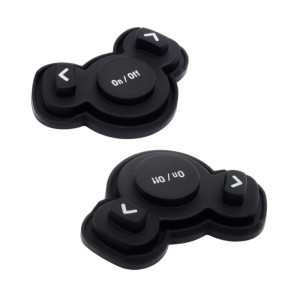
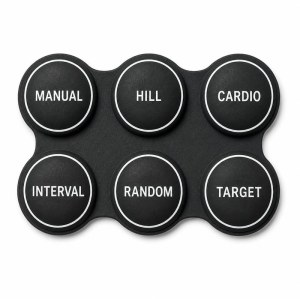
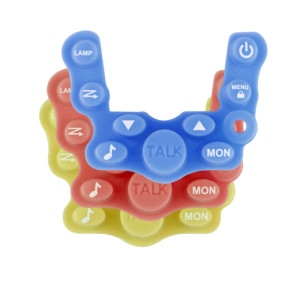
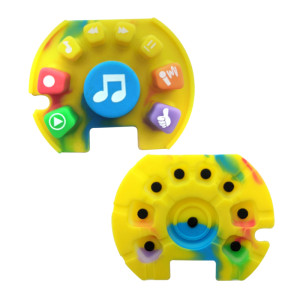
What We Mold for Industrial Equipment
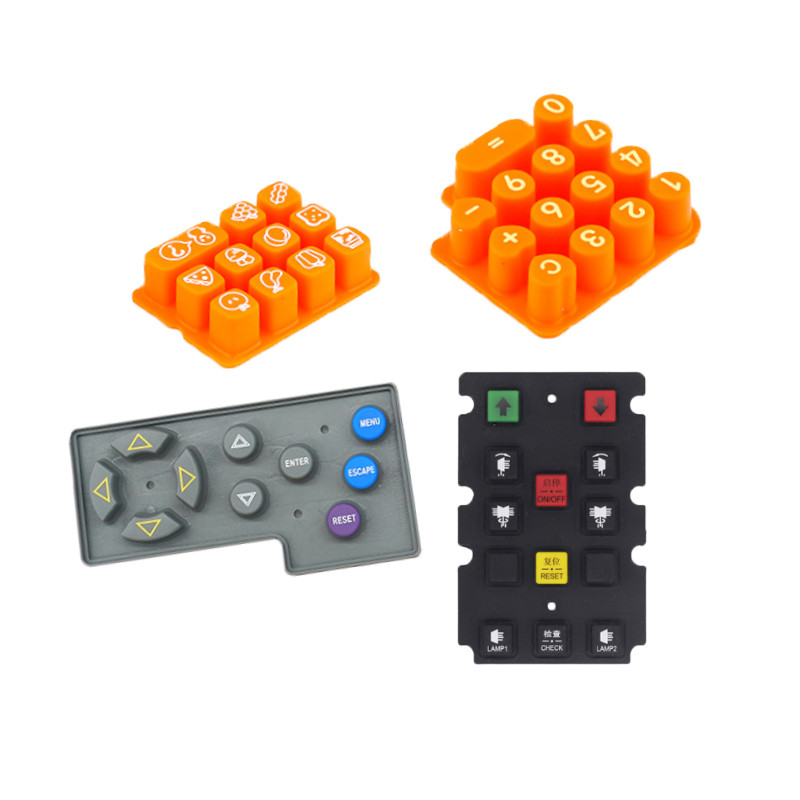
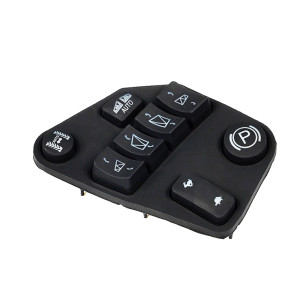
We mold silicone buttons for industrial equipment — machine control panels, handheld instruments, pendant stations, medical devices and self-service terminals. The button is what your operator touches every shift, so it has to survive oil, gloves, cleaning agents and a few million presses.
We are the factory, not a trading company. Our own tool room cuts the mold, our presses run it, and printing, laser etching and backlight assembly all happen under one roof. When something needs changing, there is no third party in the middle of the conversation.
To quote, we need one of two things: a STEP file, or the physical button you are replacing. Send either and you will have a price the same day.
6,532
Custom projects molded
7,254
Molds held in storage
92%
First-pass yield, molded
3 hours
To a written quote
Specifications We Set Before Cutting the Mold
These are the numbers an industrial button lives or dies by. We lock them down at drawing review, not after the first shot — change a durometer or a stroke once the tool is cut and you are buying a new mold.
What You Can Specify
Six things, all fixed on the drawing. Each one carries a trade-off, and we will tell you which way we would push your part.
Color
Any Pantone reference, matched in the compound rather than painted on. Multi-color keys are molded in one shot, so the second color cannot peel off the first.
Hardness
30 to 80 Shore A. Soft compound is easier on the finger but leaves burrs at the parting line. Past 70 A on a thin web, the key edge starts going brittle.
Legend
Silk screen, laser etch or double-shot. Etching cuts into the coating, so the legend sits inside the surface — what you want on a panel that sees oil and solvent.
Backlight
Translucent base at 90% transmission or better, masked to block completely at 1000 Lux. Zones light independently, so one panel can show a green run state beside a red fault state.
Structure
Keycap height, skirt, webbing angle, guide rib, carbon pill or metal dome. Add a hard plastic cap and it becomes P+R. All of it settled on the drawing.
Packing
Anti-static tray or individual PE bag, then a five-ply export carton. Tell us how your line feeds the parts and we pack to that, not to a default.
Every one of those is built on silicone compression molding with a steel tool cut in-house. If you want the wider picture of what the plant runs, start there.
How a Custom Button Is Made
1
Send a STEP file or a sample
STEP or IGS for 3D; DWG, DXF or PDF for 2D with tolerances marked. Out of drawings? Mail the button you are replacing, or the housing it sits in, and we scan it back into a model.
2
DFM review, then a quote
An engineer checks wall thickness, webbing angle, draft and the sealing face before anyone prices it. Single parts are quoted within 3 working hours; multi-process assemblies take up to 24.
3
Sample tool, first shots
Sample tool in 3–5 working days, then 5–10 pcs shipped so you can fit them on the real housing. Fit and feel are settled here, before production tooling is cut.
4
Production tooling and run
Multi-cavity production mold in 10–12 working days, mass delivery 7–10 working days after confirmation. Existing molds can sit here between runs.
Four Questions Worth Asking Before You Order
They come up in almost every first call. The answers usually decide whether there is a second order.
Are you a factory, or a trading company?
A factory. 12,000 m² in Qiaotou, Dongguan, 220 staff, 32 compression molding presses, 8 injection machines and 7 CNC centers — plus our own tool room, which is why a sample mold takes 3–5 days instead of three weeks. Come and see it, or ask for a live video tour of the line before you order.
I have no drawing. Can you still give me a price?
Yes, but not from a photo. A photo carries no dimensions and no surface geometry, so anything we quote from one is a guess that comes back to bite both of us three or four weeks later.
To price the part properly we need one of two things: a STEP or IGS file, or the physical button — worn, broken, or the housing it fits into. We scan it and rebuild the model.
Send either and the quote is straightforward. Send neither and all we can give you is a rough range, and chasing the missing dimensions is exactly what stretches these projects into months.
Who owns the mold, and who pays for it?
You own it. Ownership transfers on full payment, and you can move it, transfer it or retire it whenever you like — we just store and maintain it. Sample tooling and production tooling are quoted separately and priced to the actual cavity layout, so you are not paying for cavities you will never run. Storage and warranty run two years.
What happens if the parts are wrong?
We answer within 2 hours and remake or replace at our cost within 48, freight included, when the defect is on us. First-pass yield on molded parts runs at 92%, and outgoing lots are sampled to AQL 0.65 / 1.0 before they ship.
Inside the Plant
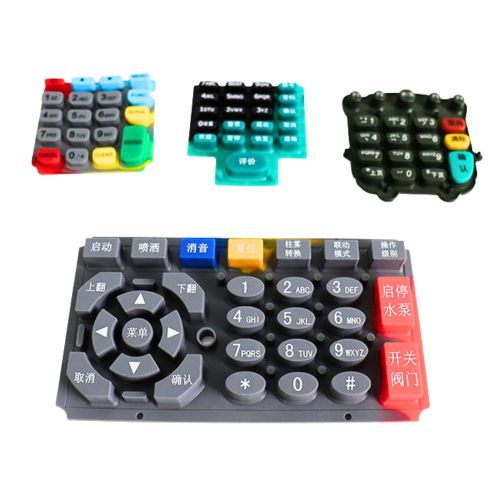
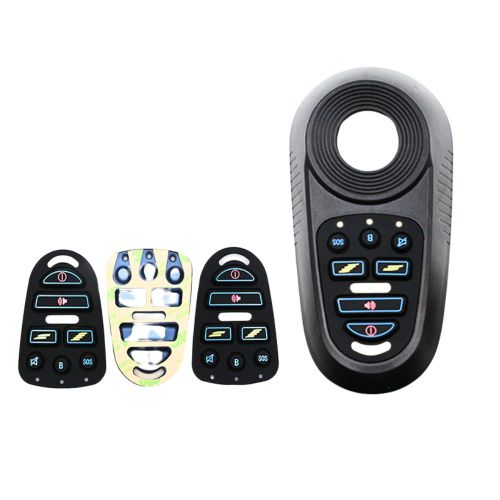
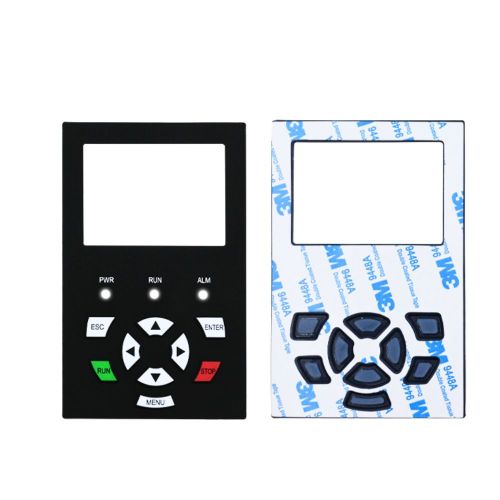
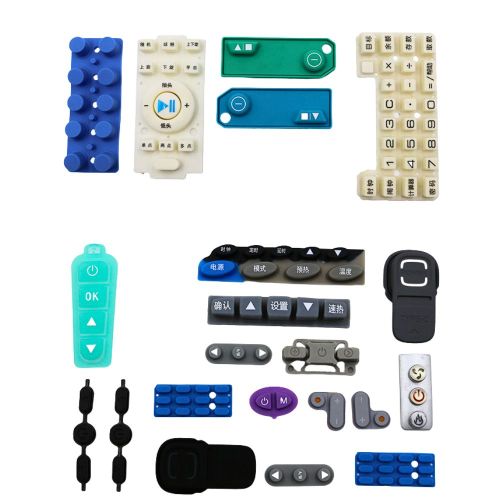
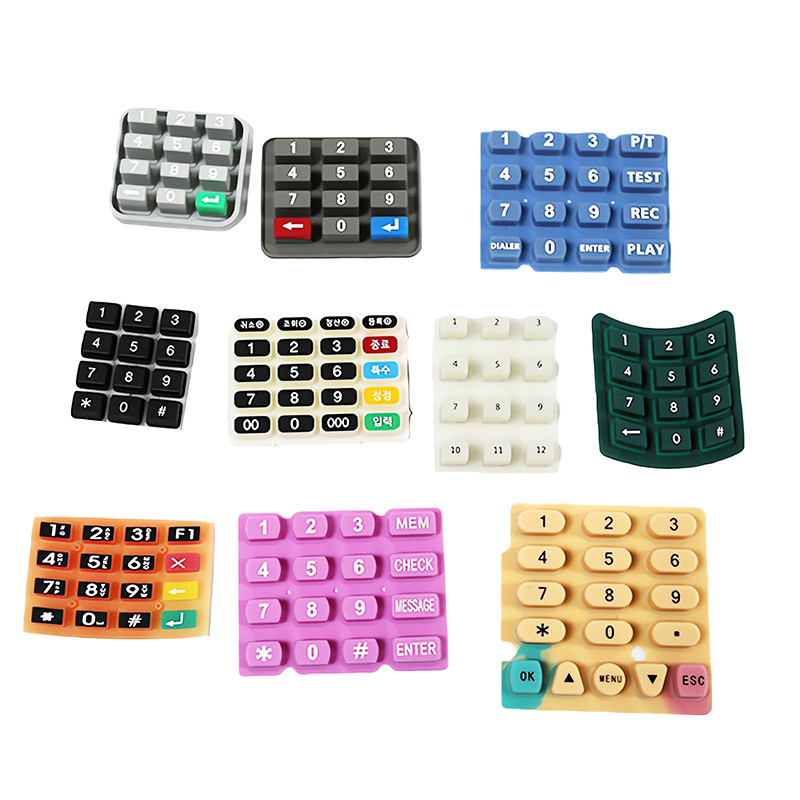
Everything here came off our own presses: multi-color keypads, bilingual legends, icons molded in rather than stuck on, and guide ribs for gloved hands.
Tooling, molding, trimming, printing, laser etching, backlight assembly and packing all sit under one roof. That is what makes a 3-hour quote and a 3–5 day sample realistic rather than optimistic.
The certificates are not decorative. Raw material arrives with a COA per batch and is re-tested for hardness and tensile strength before it reaches a press — details under raw material certification, with the full set available to download before you order.
Where These Buttons Are Used
All of these came out of the same process. What changes is the tool, not the material — numeric pads, function clusters, curved keycaps and bilingual legends are driven by the housing, not picked from a catalogue.
Machine control panels
Machine tools, packaging lines, woodworking equipment. Coolant and chips are what kill a legend, so it gets etched, and the panel gets a sealing skirt instead of a flat gasket.
Handheld instruments
Meters, analyzers, calibration tools. Low press force and a short stroke, because the operator is working one-handed with a thumb.
Construction and agricultural machinery
Pendant stations, joystick overlays, dash panels. Vibration and gloves set the spec: long travel, a guide rib, and a 3–5 million cycle rating.
Medical devices
Diagnostic equipment and patient-handling controls. Cleanability matters more than force, so the surface gets a PU or matte coat that stands up to repeated wipe-down.
POS and self-service terminals
Payment terminals, kiosks, access control. Public use means the legend has to survive thousands of presses a day from people who do not care about the machine.
Home appliance controls
Coffee machines, ovens, air treatment. Color and backlight carry more weight than cycle count here, and P+R is often the right construction.
Samples in 3–5 Days, Tooling in 10–12
3 h
Written quote on a single part
3–5 days
Sample mold and first shots
10–12 days
Production mold
7–10 days
Mass delivery after confirmation
What to put in your first message
With a drawing: STEP or IGS, or DWG/DXF/PDF with tolerances marked. Without one: mail the button you are replacing, or the housing it fits into. A photo on its own will not produce a price — we need something we can measure.
Also useful: durometer if you know it, the cleaning agents the machine sees, whether the operator wears gloves, and your annual volume. Missing details are fine — we will ask.
Frequently Asked Questions
30 Shore A or 70 Shore A — which do I need?
Start with the press force you want, then let the durometer follow. On a fixed webbing thickness, every 5° of added hardness raises peak force by roughly 15–25%. Below 40 A the key recovers slowly and feels sluggish. Above 70 A on a thin web, the edge turns brittle.
Should the legend be laser etched or silk screened?
Etch it when the panel sees oil, coolant, solvent or heavy thumb traffic — the legend sits inside the coating instead of on top of it. Silk screen is cheaper and fine for decorative color on a clean, dry panel.
Will the button survive the cleaning agents on my machine?
The silicone body handles common shop chemicals, but the coat and the housing seal decide the answer. Tell us which agents are used and we will match the finish before tooling, not after the first complaint.
Can different keys on one panel light up in different colors?
Yes. Masked channels block completely at 1000 Lux, so a single panel can show a green run state next to a red fault state without light bleeding between them.
Can I run a small trial batch first?
1,000 pcs is the standard minimum, but a 100 pcs trial run can be approved so you can fit the part on real machines. That is usually cheaper than finding a fit problem after a full run.
What makes a key feel crisp instead of mushy?
The webbing angle and thickness, not the durometer alone. A click ratio between 40% and 55% reads as crisp on a control panel. Flatten the web angle and the snap disappears, even at the right hardness.
Send a STEP File or a Sample. Either Gets a Price.
- With a drawing: STEP or IGS, or DWG/DXF/PDF as a ZIP
- Without one: mail the old button or the mating housing — we scan it and rebuild the model
- A photo alone will not produce a price. We need something we can measure
- Quote within 3 working hours. Sample tool in 3–5 days. The mold is yours