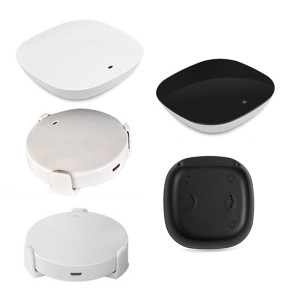
Custom Inject Plastic Enclosure - Pre-Drilled Holes for Connectors & Displays
- Model
- BH-Plastic Enclosure
Item specifics
- Design
- Follow 3D Drawing Or Physical Object
- Process
- Injection Molding
- Feature
- Secure & UL94
- MOQ
- 1000pcs
- Application
- Connector Cutouts Pre-Drilled
Review
Description
Enclosure engineering Every hole drilled after moulding costs a fixture, a setup and a tolerance band. Moulding them in holds ±0.15 mm across the run and takes drilling, tapping and deburring out of the routing: 1.0–25.0 mm through holes, M3–M12 threads, display windows and vent grids in the same shot. The list is longer than most drawings assume. If a feature can be formed by a core pin, a slide or an insert, it can usually be moulded in: Being honest about the limits saves a tooling round. Cross holes that intersect at an angle the slide cannot reach are machined. Threads finer than M3, knife-edge ports and holes within about 1 mm of the parting line are better drilled. Deep bores with a length-to-diameter ratio above roughly 4:1 need a core that will not deflect, and at that point a secondary operation is usually cheaper than the tooling. Moulded-in features add around 5–15 % to the part price and nothing per hole afterwards. Post-machining adds 25–60 % to the unit cost, plus 5–15 days in the routing, plus a wider tolerance band — typically ±0.25 to ±0.5 mm against ±0.15 mm from the mould. The crossover is usually a few thousand units; below that, a standard box with drilled holes is the rational choice and we will say so. Prototypes run in aluminium tooling, production in P20 steel, and hole patterns are cut as modular inserts. That matters more than it sounds: a connector change six months into production becomes an insert change rather than a new mould. Presses run from 80 to 800 tonnes, which covers everything from a handheld instrument case to a floor-standing control cabinet. Quality is closed out with first-article inspection, CMM data on every moulded feature and functional gauges for the connector interfaces. If your assembly line uses a go/no-go check, we can build the gauge to the same drawing. A pre-drilled enclosure is quoted from the model and the connector list. Send both and the DFM report comes back with the features that should stay machined marked on it. Dongguan Bohao Electronic Technology Co., Ltd. IATF 16949:2016 / ISO 9001:2015 certified. Values shown are typical for the listed compound or platform; the drawing and the approved sample govern production.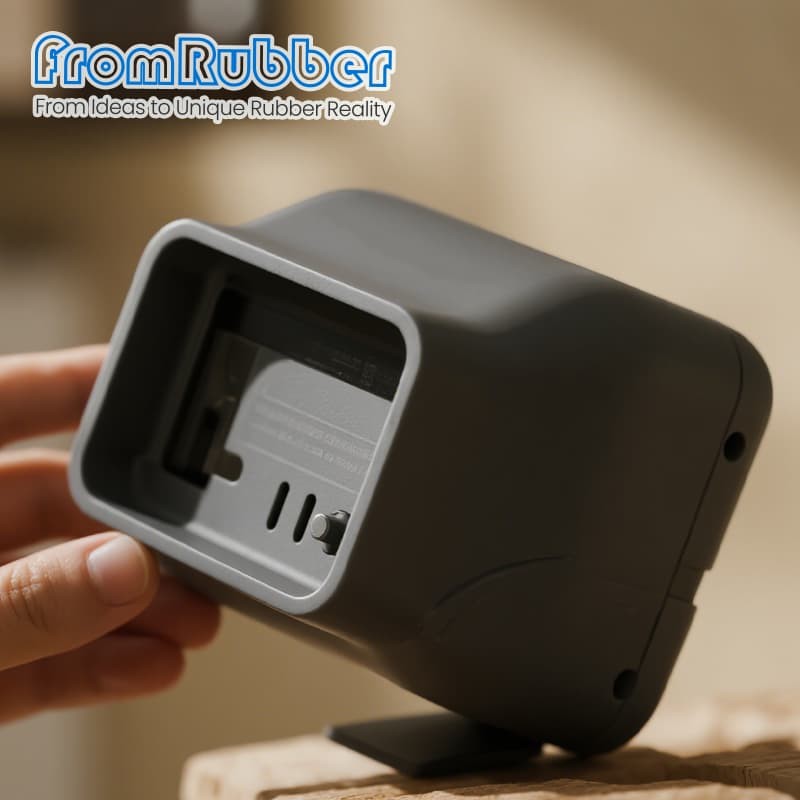
Moulded-in holes and threads, instead of a second machining step
What can be built into the tool
Feature Capability on this platform Through holes 1.0–25.0 mm diameter, ±0.15 mm Threads Moulded M3–M12, or ultrasonic and heat-staked inserts Display windows Rectangular, circular or free form, with moulded lenses Ventilation Louvers, mesh patterns and slots Connector cutouts DB9, DB25, USB, HDMI, RJ45, BNC, SMA Cable entries Strain-relief grooves and grommet seats Mounting Bosses, fan posts and standoffs What still has to be machined
The economics, stated plainly
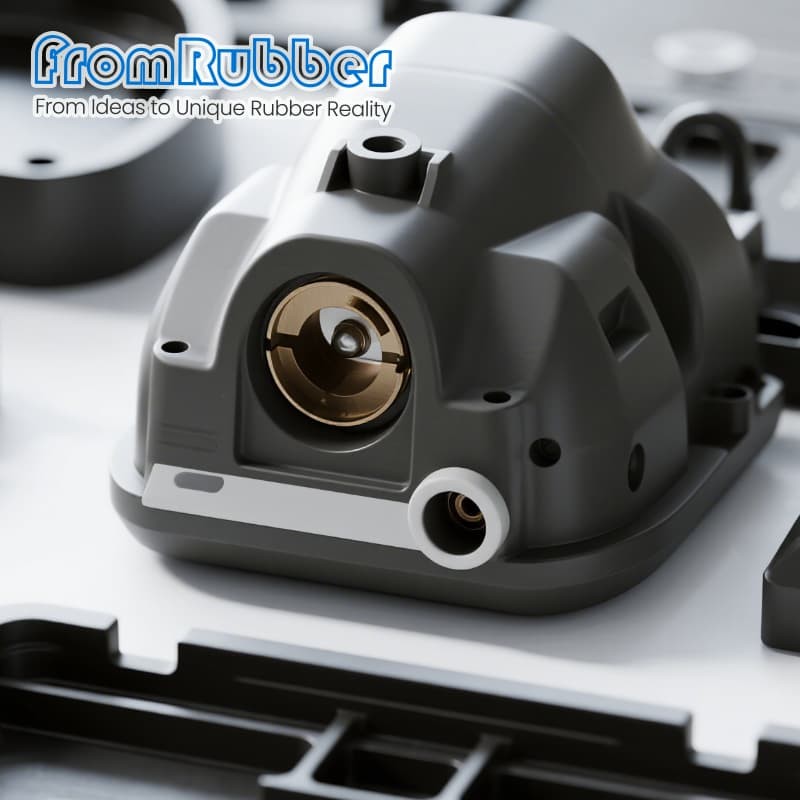
Tooling strategy
How the project runs
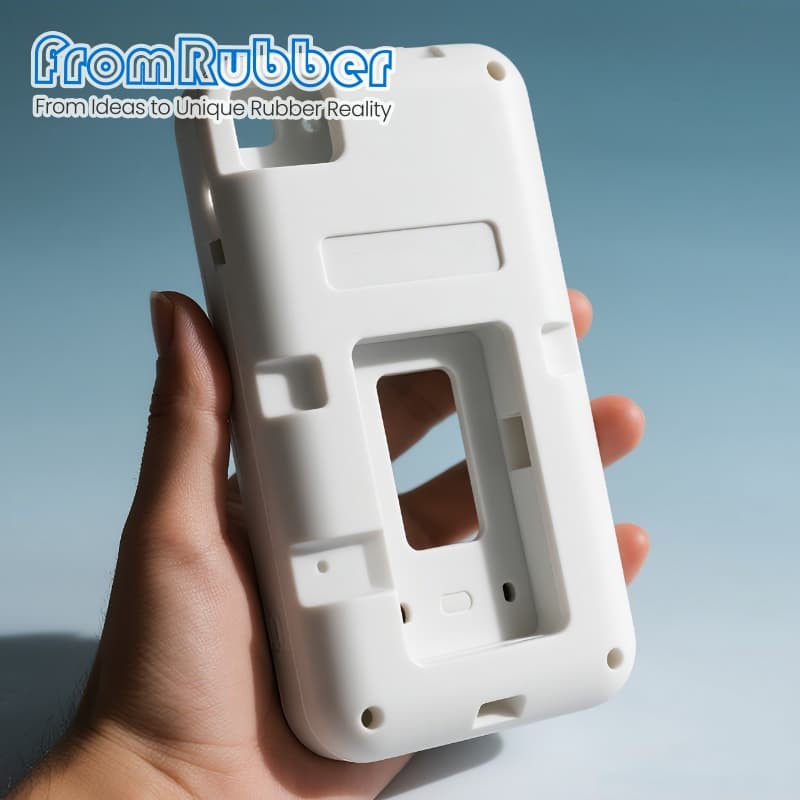
What we need to quote
What comes back
Send the STEP file with the hole callouts
fromrubber.com
+86 18926836960